01
The line first
A handsome screen does not finish the job if the cycle does not hold. Decisions are made at shift tempo.
About
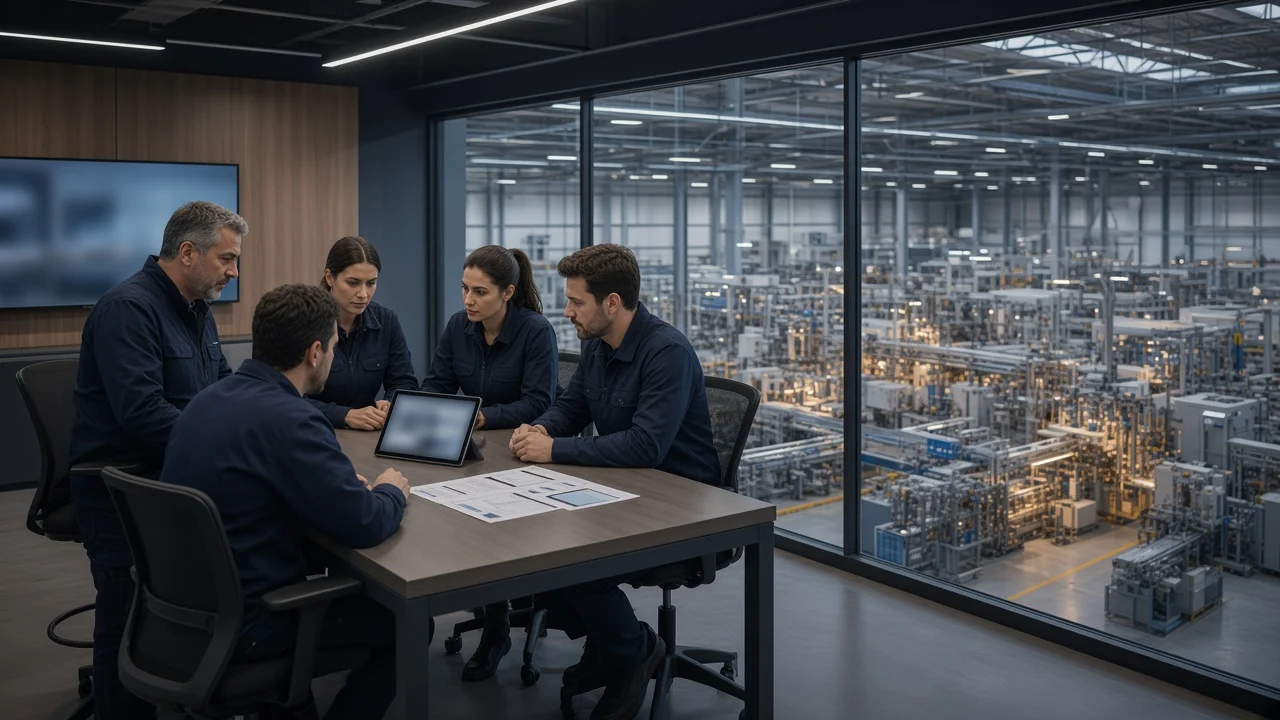
Robotics, control, and data are not separate jobs. They are one system locked to the line rhythm.
Company
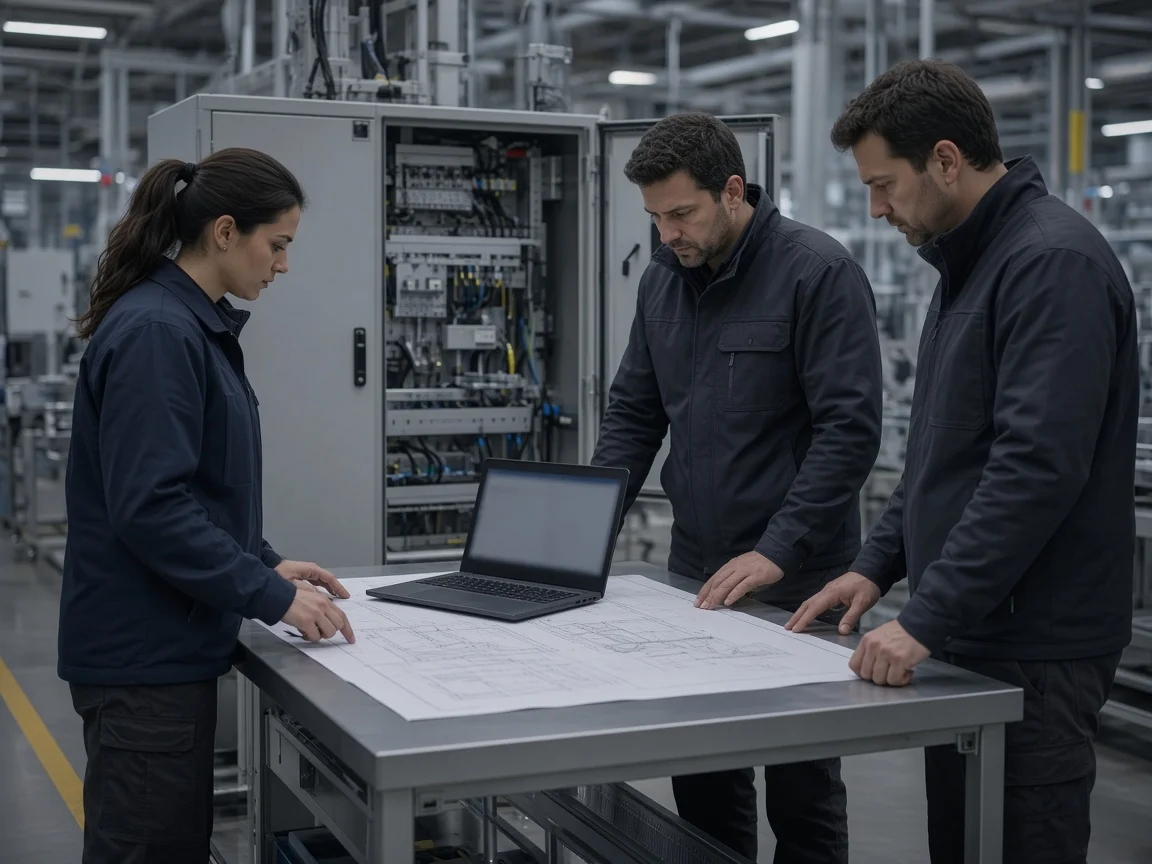
SENKRA is an Istanbul-based industrial automation team. A robot cell, line control, and production record are not separate supply lines; they are built as one line that works together.
Most of the work does not finish in the drawing room. Software is not written until the existing cycle, safety envelope, and operator habit are read on site. The cabinet, path, and screen are handed over once they share one lock.
The same rule holds on automotive supply, food, packaging, custom machinery, and electronics assembly lines: readable control, a measurable cycle, a traceable decision.
Approach
01
Cycle, safety, and operator habit are not assumed at a desk. The line is measured on the floor first.
02
Electrical, software, and motion are not separate work orders. The drawing does not close until they share one lock.
03
FAT first, then production tempo. We leave the line verified, not hurried.
04
A handover sheet is not the end of the work. The first shifts and the first stops are watched together.
Capability
Expertise is not a brand count in a catalogue. It is the cell, line, control, vision, and record speaking the same tag language.
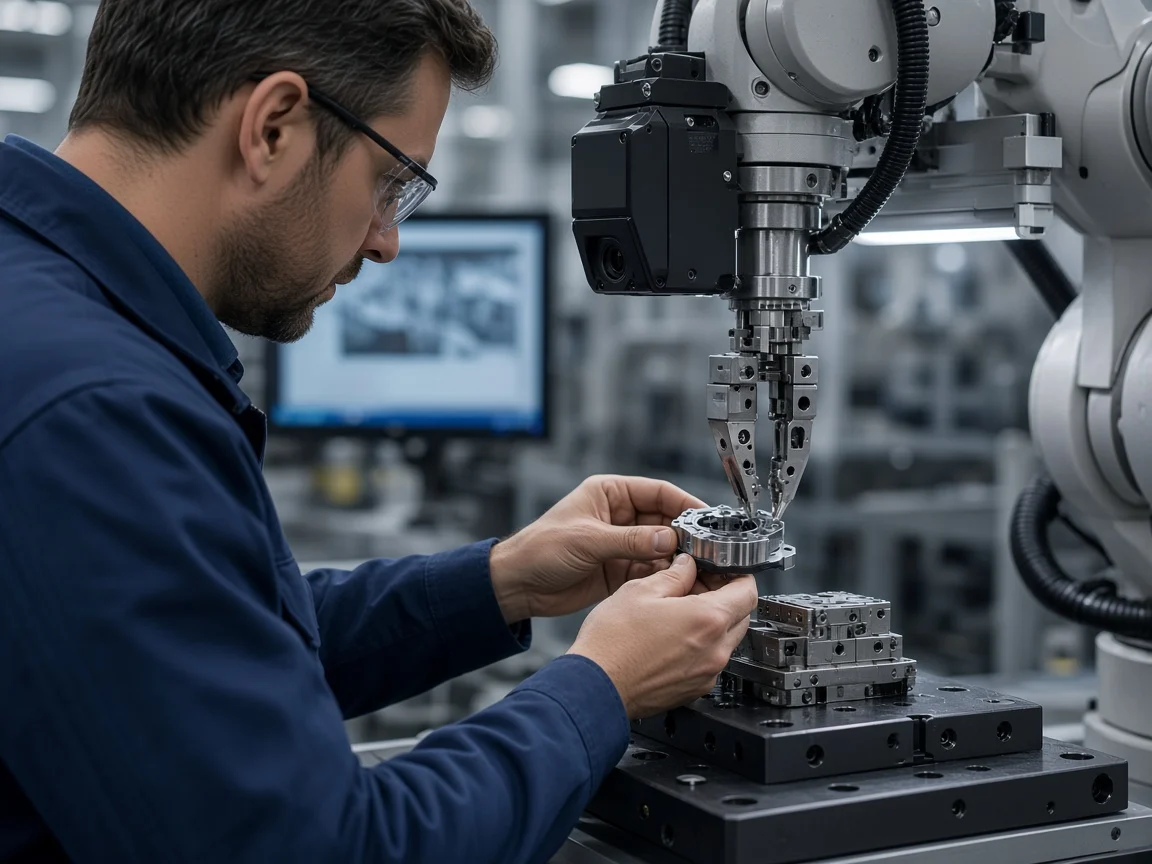
Path, tool, and safety envelope lock into the same cycle package.
Transfer, interlock, and station order are built as a measurable flow.
PLC, HMI, and alarm hierarchy are written in a language the next shift can still read.
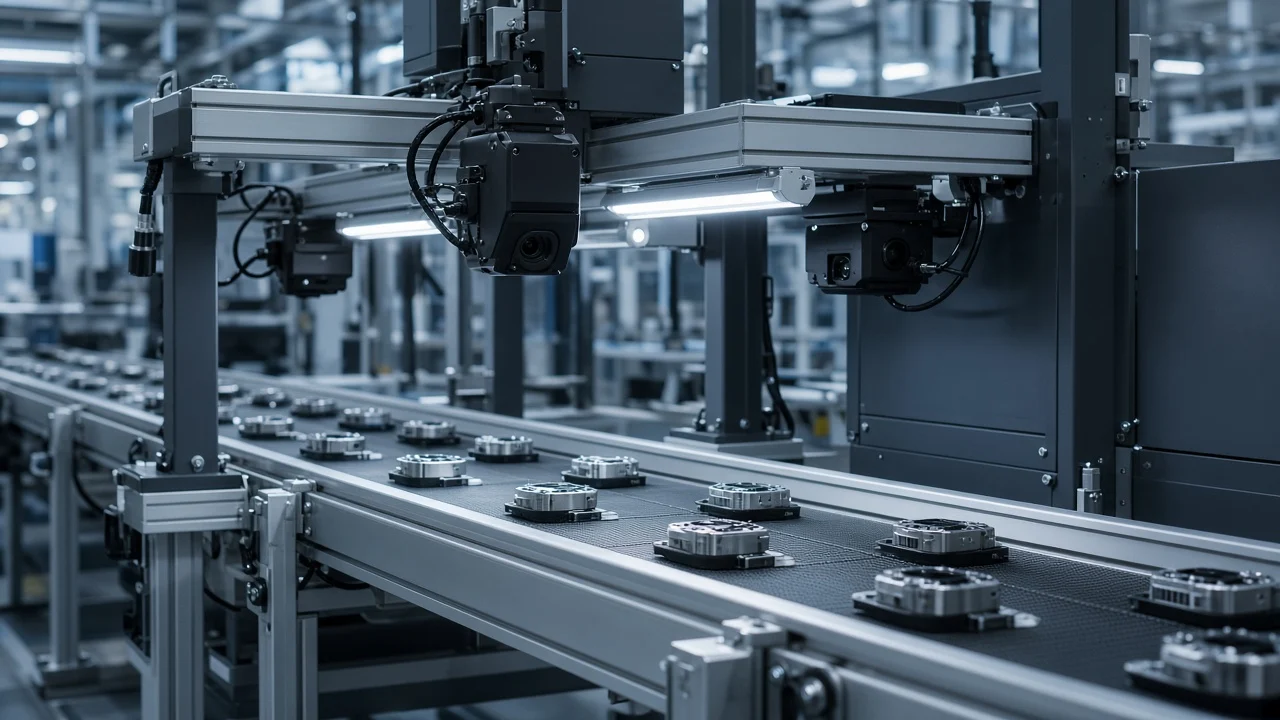
Camera, lighting, and threshold run in the same station, at line speed.
Downtime, quality, and traceability are not cut away from the control layer.
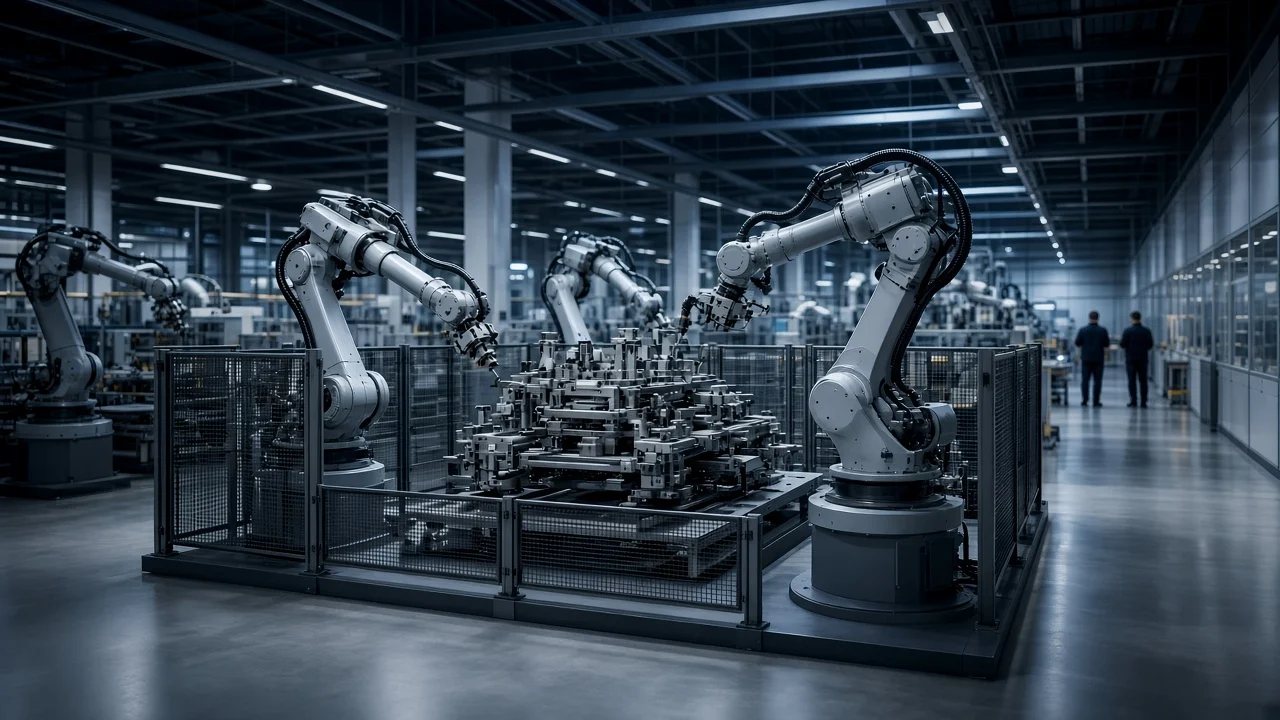
Not filling the plant; making the line measurable.
Scale
Service areas
From robotics to retrofit
Engineering disciplines
Locked at one table
Industry focus
By line rhythm
Control language
From cell to data
Principles
01
A handsome screen does not finish the job if the cycle does not hold. Decisions are made at shift tempo.
02
Software belongs to the night shift, not to the person who wrote it. Tags, alarms, and recipes stay plain.
03
Simulation speeds the desk. The real lock is thrown when the part enters the line.
04
When commissioning ends, the line is not left without an owner. The first stops are read together.
Industries
Contact
Cell, line, or retrofit. We lock which job comes first without stopping the plant you already run.