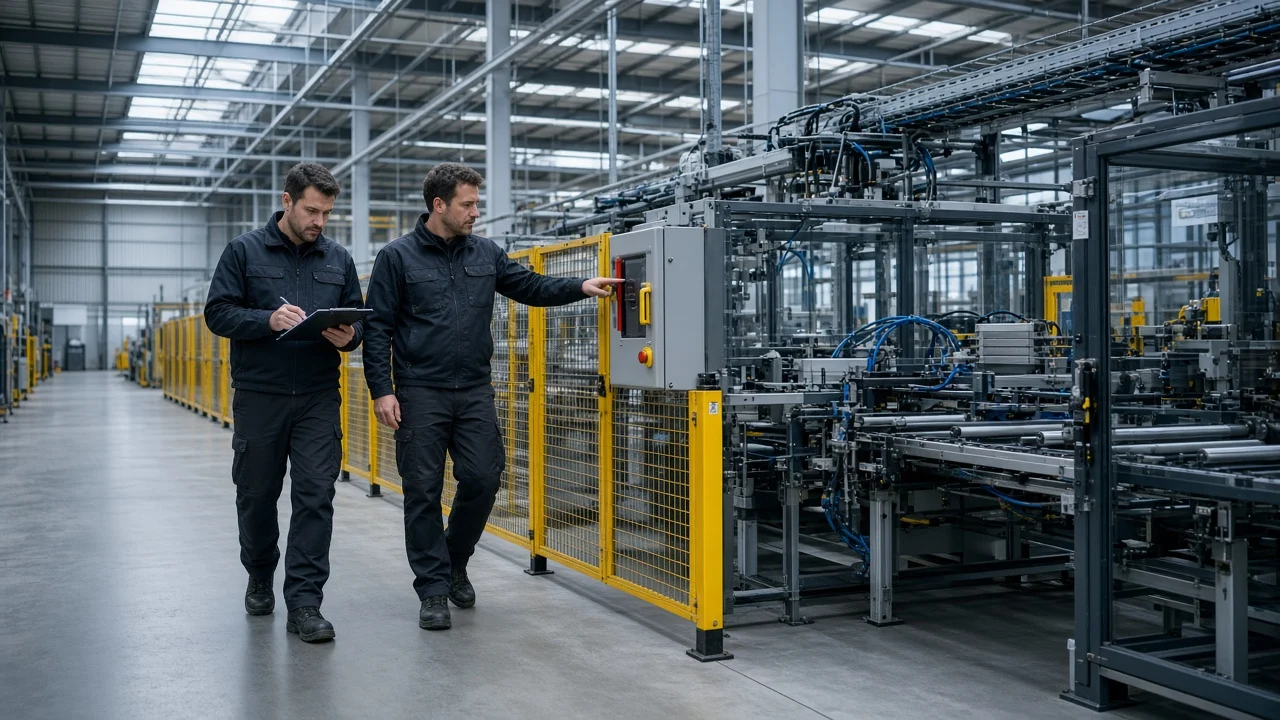
Two engineers reading a transfer and a safety gate on the production line

How we work

A quote is not written
before the line is read.

Six locks from first contact to SAT. The work done, the document that comes out, and the decision taken with you sit in one language at every stage.

How we work

First contact is not a quote slide.

The customer arrives with a stuck job first: leftover assembly, a broken pallet, an aged cabinet, or a late defect. A service is not picked from a catalog.

Reading, scope, architecture, integration, FAT, and SAT sit at the same table. If a stage is skipped, the line still runs on a guess.

  1. 01Line reading
  2. 02Scope lock
  3. 03Architecture lock
  4. 04On-site integration
  5. 05FAT
  6. 06SAT and first shift
Two engineers reading a safety gate and transfer on the production line
01 · First contact

01 / First contact

Line reading

It is not assumed at a desk. Cycle, gates, and operator habit are measured on site.

Work
Existing transfer, safety envelope, I/O boundary, and stoppage habit are read on the floor. Cell, line, vision, or retrofit — which one is stuck becomes visible here.
Output
As-is line note: part path, lock points, downtime window, and neighboring interface.
Decision
Which job comes first. No quote is written until the scope draft is locked.
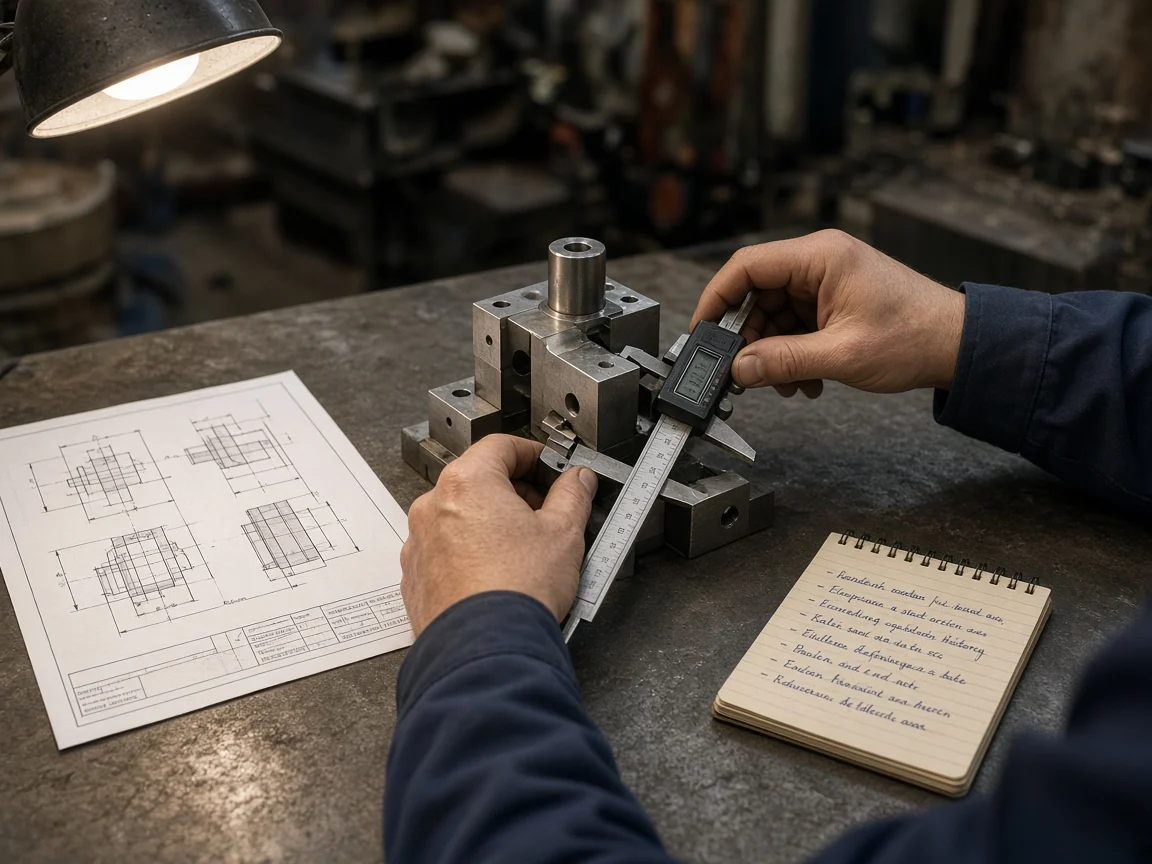
Engineer locking scope inputs with a drawing, a fixtured part, and a caliper

02 / Boundary

Scope lock

In-scope and out-of-scope sit in the same sentence. A brochure item is not a scope.

Work
Station boundary, safety envelope, recipe field, and neighboring-line handshake are written. Downtime window and FAT draft go in the same package.
Output
Locked scope package: boundaries, interface, success rule, FAT item draft.
Decision
In-scope / out-of-scope and which shift the intervention happens on are confirmed with the customer.
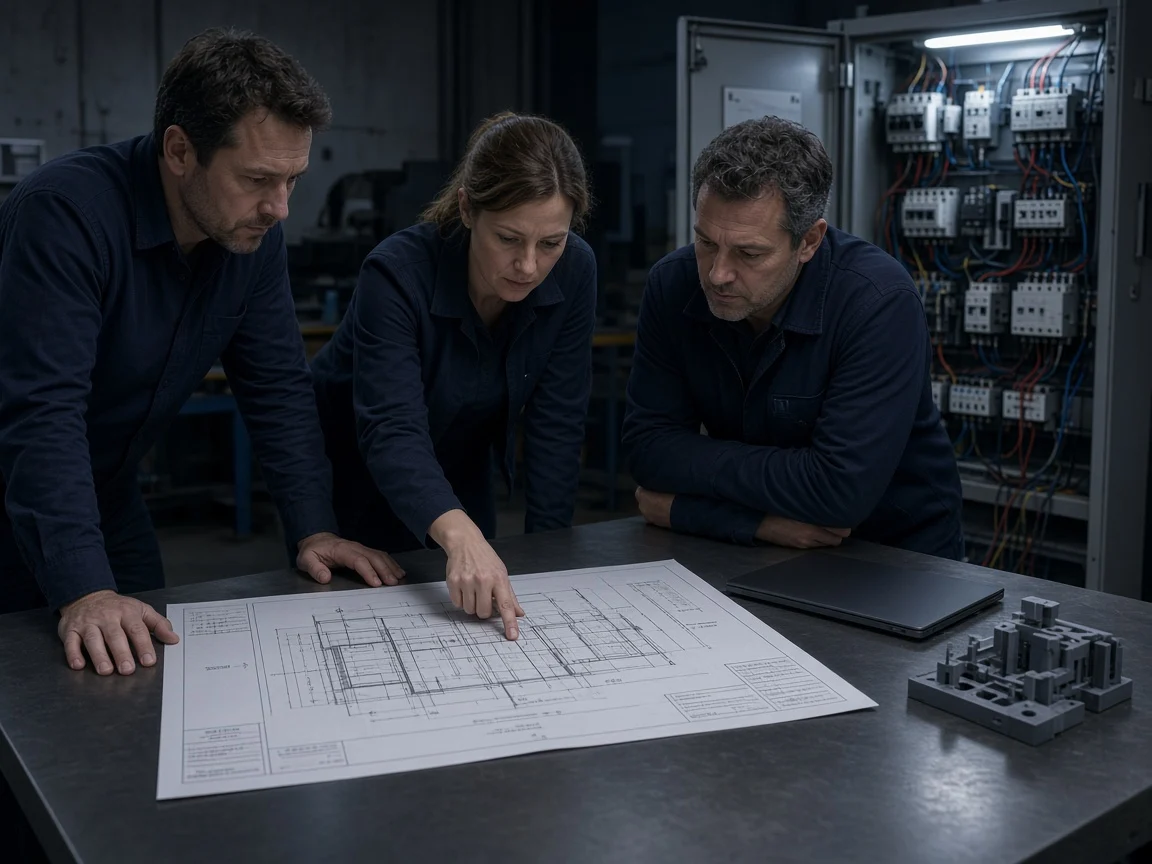
Engineers discussing the architecture lock over a cell layout drawing and fixture mock-up
03 · Design

03 / Design

Architecture lock

Not an interface — a lock is drawn. Electrical, software, and motion sit in the same tag language.

Work
Cabinet and I/O map, safety PLC layer, cell layout, path envelope, and HMI glossary lock at the same table.
Output
Tag glossary, I/O map, layout, and safety envelope. Simulation does not stay on the desk; the language that will bind to the floor is extracted.
Decision
Control language, safety layer, and path assumption are approved together. Assembly does not start until the drawing closes.
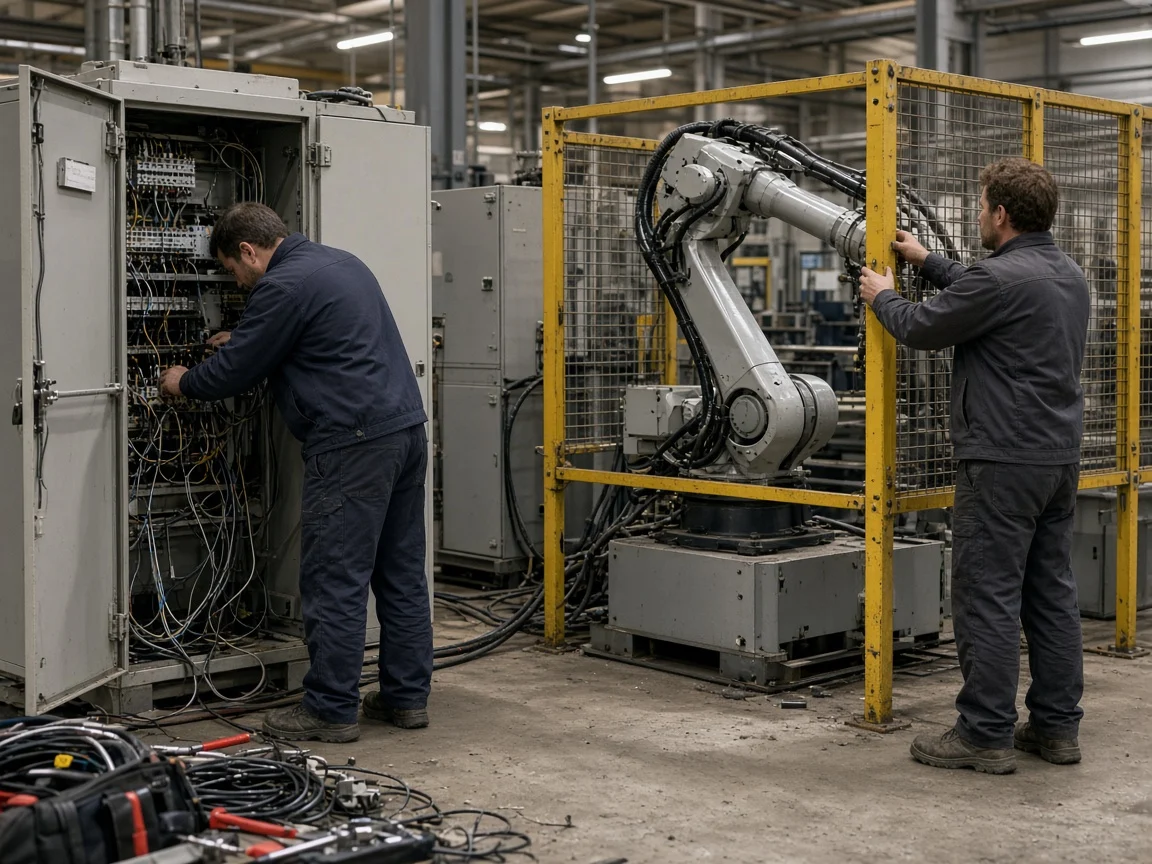
Two engineers integrating a robot cell with safety fencing and an open cabinet

04 / Installation

On-site integration

Cabinet, cell, and transfer do not sit in separate boxes. The connection is made on the line.

Work
Cabinet, robot, gripper, vision station, and line lock are connected on the floor or in a controlled area. Cabling and safety fencing move in the same sequence.
Output
Connected system: power, I/O, motion, and gates seat on the same lock.
Decision
Exit to the FAT list. “It works” is not said while the list is open.
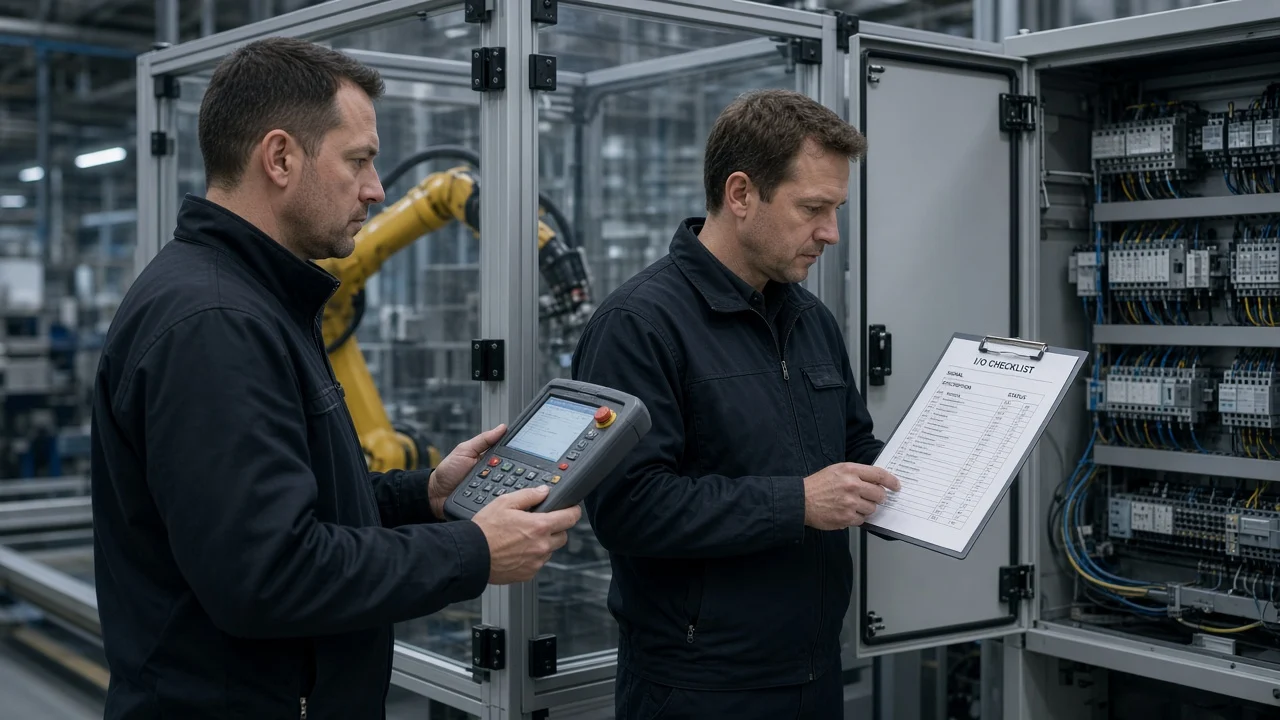
Two engineers verifying a cell at FAT with a teach pendant and I/O list
05 · Verification

05 / Verification

FAT

A guess does not close. I/O, gates, recipes, and paths close item by item.

Work
Terminals, e-stop, reset, gripper release, and vision threshold are verified at a controlled pace. An island test is counted incomplete if neighboring transfer is missing.
Output
Closed FAT list and teach record. No shipment with open items.
Decision
Exit to site or move to SAT. The customer signs the list together.
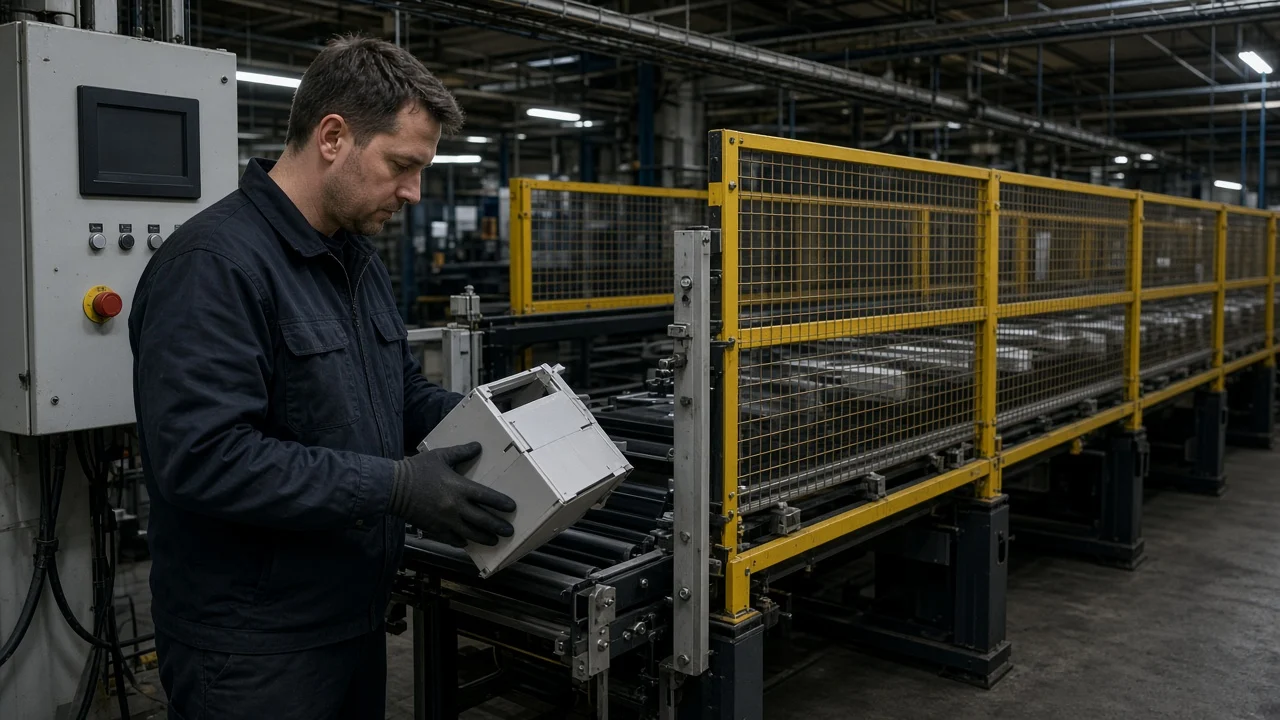
Engineer watching SAT by checking a part leaving beside the transfer line

06 / Handover

SAT and first shift

Line rhythm is locked on the production floor. The day after sign-off is still part of the job.

Work
Neighboring transfer, operator habit, and recipe change are watched at production tempo. First stoppages are read together.
Output
A line running at SAT, updated HMI, and a first-shift note.
Decision
Handover closes. The first alarm and recipe drift are not left as “your problem.”

Related services

The process is the same. The door is the line.

All services
  1. 01Robotic Automation

    A robot is not a cell until it locks to the line rhythm.

  2. 02Line Automation

    A running station is not a running line.

  3. 03PLC & SCADA

    Control software must belong to the night shift as well.

  4. 04Machine Vision

    A camera is not a quality system. The station is.

  5. 05Retrofit

    Sound mechanics do not have to be stripped out.

Engineers talking through the architecture lock over a cell layout drawing

First contact

Let’s read the stuck work together.

Cell, line, vision, or retrofit. Scope comes from the work sitting on your line, not from a catalogue.

Full request form