Projects / 06
The sequence runs
without fighting cleaning.
The stations were running; after cleaning the line had to be rediscovered. Sequence was tied to the hygiene window.
Project
Filling Line Transfer Lock
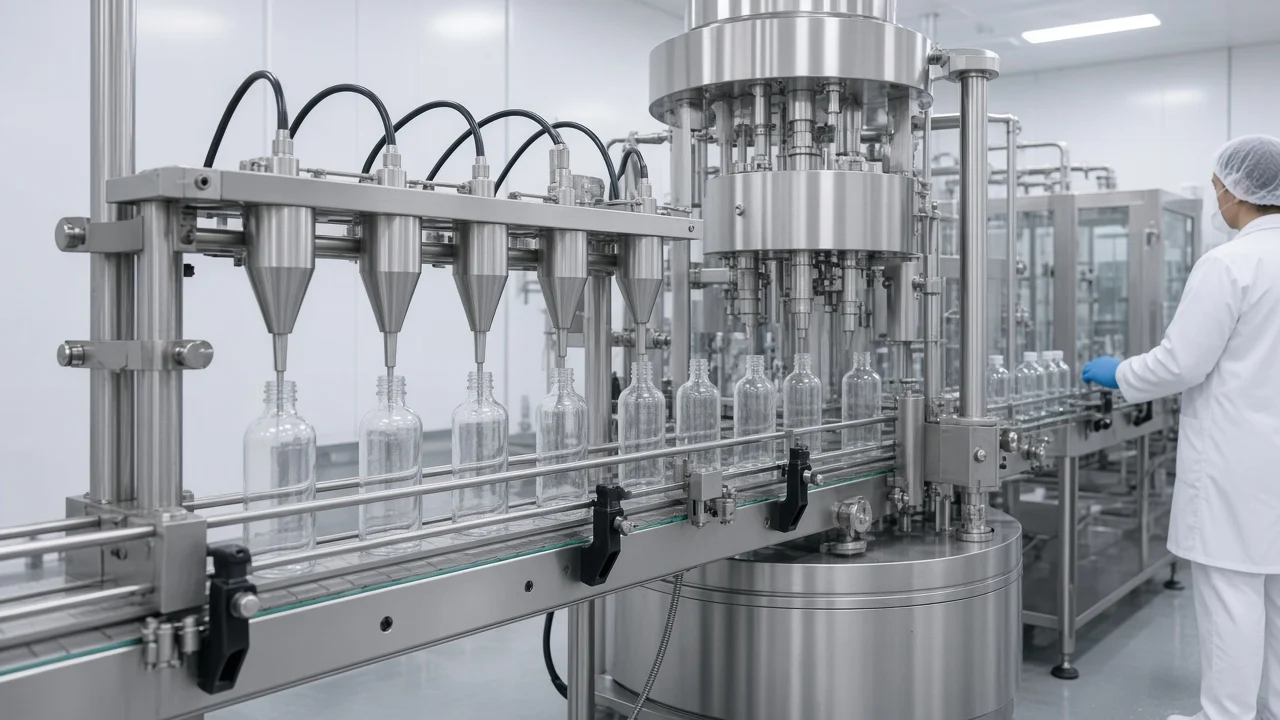
In the Balıkesir hall, fill and cap spoke different languages. After cleaning, the line had to relearn the sequence.
Laying conveyors was not enough. The reason for a stop had to sit in the same tag vocabulary as the hygiene window.
Need
If reset overrides hygiene, the line is rediscovered.
The stations were running. The real break was that the shared interlock ran on guesswork.
01
Sequence is broken
Fill finishes; cap runs on its own tempo. Transfer disappears in between.
02
Cleaning is a stranger
The CIP window is not part of the reset logic.
03
Level arrives late
An underfill shows at the next point — sometimes on the shelf.
Approach
The sequence talks to cleaning.
The reason for a stop was separated first. Then transfer and the vision decision were written into the same flow.
- 01
Sequence
Fill, weigh, and cap locked in one line language.
- 02
Hygiene
The cleaning window is part of reset, not a stranger to it.
- 03
Decision
Level and cap presence go to the PLC at line speed.
Scope
What locked on this job.
- 01
Fill, weigh, and cap sequence
- 02
Transfer and buffer interlock
- 03
Reset logic with the cleaning window
- 04
Level / cap vision decision
- 05
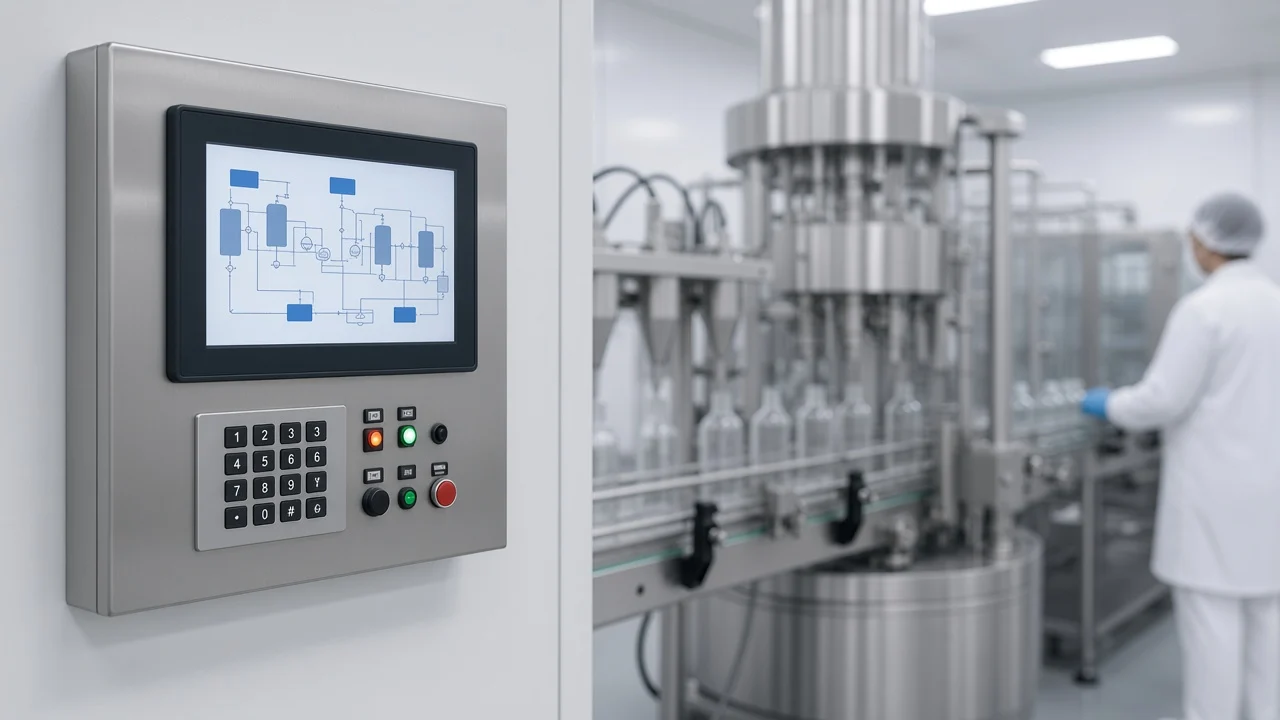
HMI recipe and access
Application
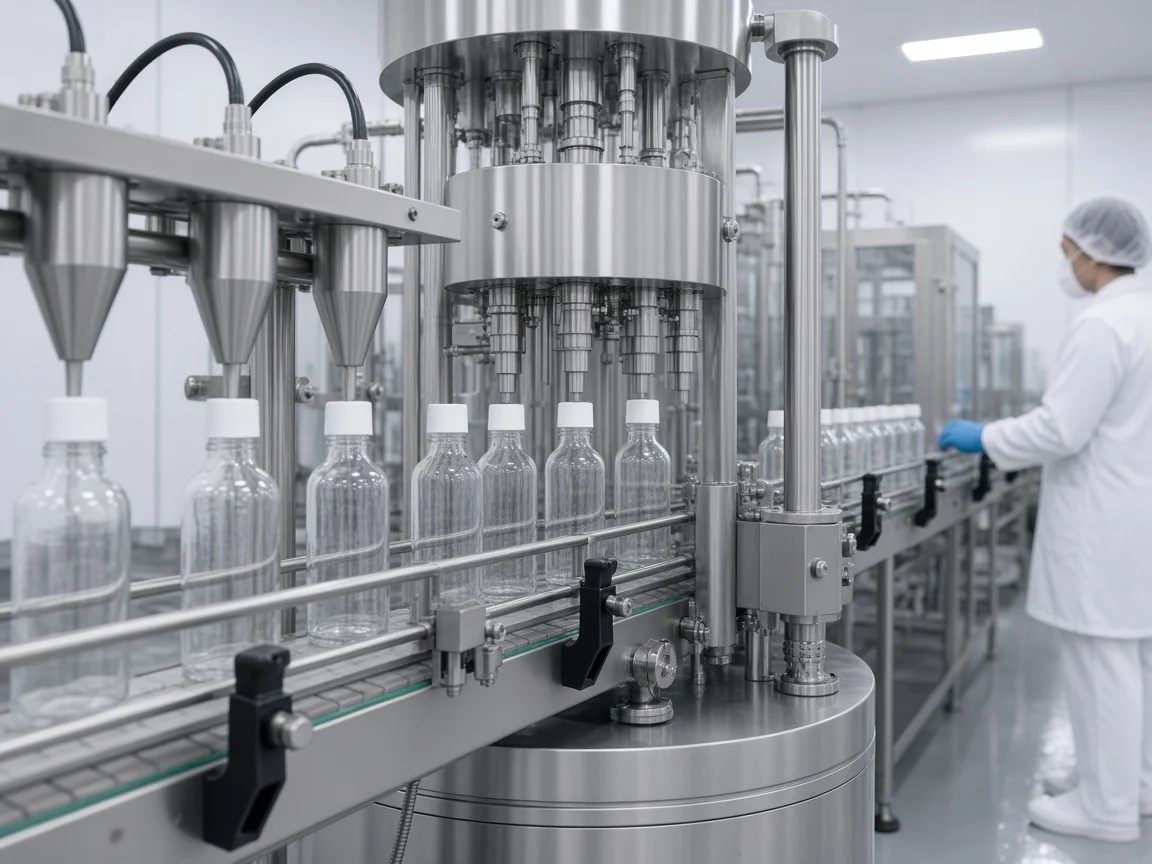
Hall, turret, screen.
03 frames
01 / 03
On site
The cap continues the fill.
When the recipe changes, the sequence changes with it. A fail leaves without blocking the line. The HMI belongs to the night shift.
Services
Services used.
- 02Review
Line Automation
A running station is not a running line.
- 03Review
PLC & SCADA
Control software must belong to the night shift as well.
- 04Review
Machine Vision
A camera is not a quality system. The station is.
Result
The sequence is the hall’s language.
We do not invent a fill rate or a scrap percentage. Delivery is a flow that talks to hygiene.
New production flow
Fill, cap, and cleaning sit in the same interlock.
Integrated system
The level decision is tied to the PLC; the recipe to the HMI.
Process scope
Reset does not ignore the cleaning window.
Projects
Talk with the engineering team.
A new line, an existing cell, or an ageing cabinet. Scope comes from the work on your line, not from a catalogue.