Projects / 03
The fault stays at the station,
not at the customer.
There was a camera. There was no station. Light, trigger, and pass-fail locked on the same bench.
Project
Vision Quality Inspection
A camera had been bought on the Eskişehir assembly line. Thresholds written before lighting was installed drifted every shift; a pin fault showed up at the next gate.
A station is not a lens count. Until lighting, trigger, and the PLC interlock sit on the same bench, the decision arrives late.
Need
A fault missed by eye is at the next gate.
The request arrived as “a better camera.” The real gap was that the station did not measure.
01
Threshold depends on the shift
A tolerance written under poor light was rediscovered every shift.
02
Decision on an island
Vision said yes or no; the press or line interlock did not listen.
03
Record is detached
The code was read; traceability stayed in a separate file.
Application
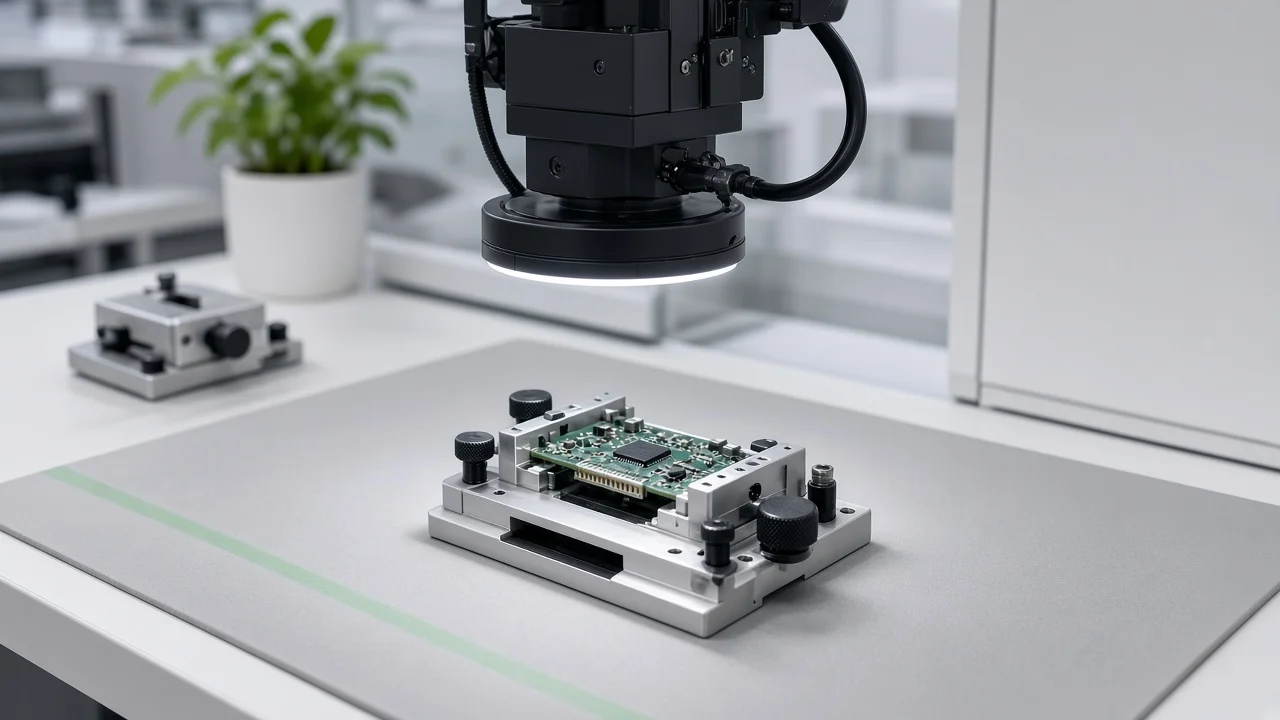
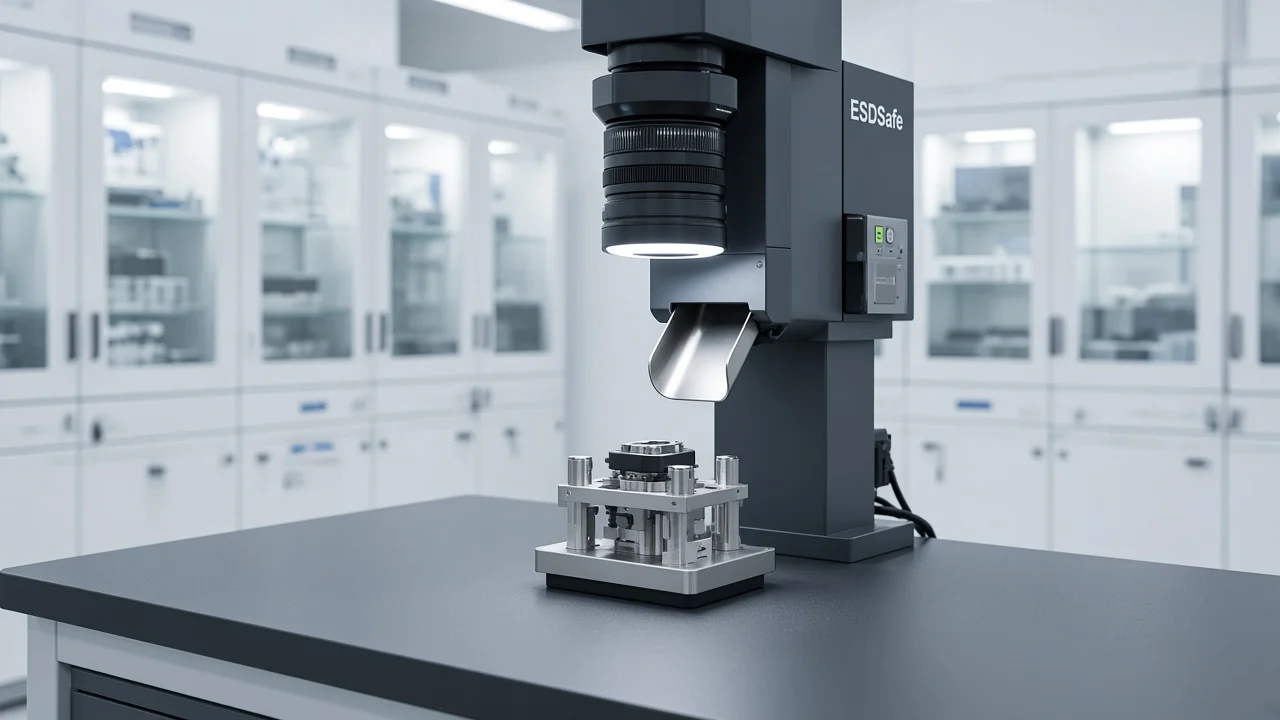
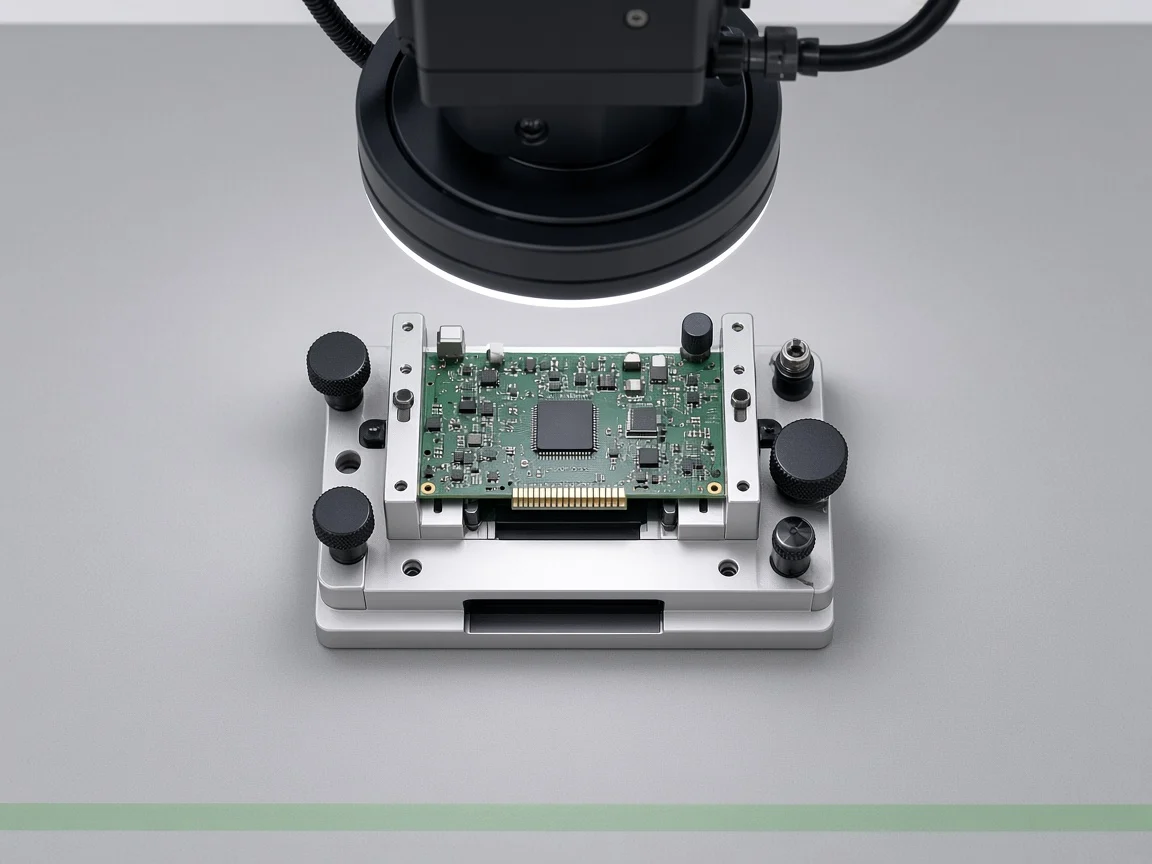
The station is visible before the camera.
03 frames
01 / 03
Approach
Light first, then the threshold.
An algorithm will not rescue poor lighting. The bench was built before the camera.
01
Light
Ring lighting was wired to make the defect repeatable, not to inflate it.
02
Trigger
The image locked to line speed. A late frame is not a decision.
03
Interlock
Pass-fail went to the PLC. A fail leaves without blocking the line.
Scope
What locked on this job.
- 01
Station fixture and part seating
- 02
Controlled ring lighting and camera
- 03
Trigger sync at line speed
- 04
Pin, position, and presence thresholds
- 05
PLC pass-fail interlock and traceable record
On site
The fail stays on the bench.
Pin and seating are measured. The decision drops with the record. The next station does not wait for a suspect part.
Services
Services used.
- 04Review
Machine Vision
A camera is not a quality system. The station is.
- 03Review
PLC & SCADA
Control software must belong to the night shift as well.
Result
The decision is the station’s output.
We do not claim a percentage of faults reduced. Delivery is a measurement package locked to the line.
Commissioned solution
Lighting, trigger, and threshold run on the same bench.
Integrated system
Pass-fail goes to the PLC interlock; the record drops with the code.
Process scope
Pin, position, and presence are measured at line speed.
Projects
Talk with the engineering team.
A new line, an existing cell, or an ageing cabinet. Scope comes from the work on your line, not from a catalogue.