Projects / 02
The pallet is the line’s work,
not the end of the line’s.
We made the pallet the line’s work, not the end of the line’s. Stacking, stretch, and transfer speak in the same sequence.
Project
Palletizing Automation
In the Çorlu packaging hall, stations finished the box and the pallet could not keep up. Uneven stacks at shift end left dispatch behind.
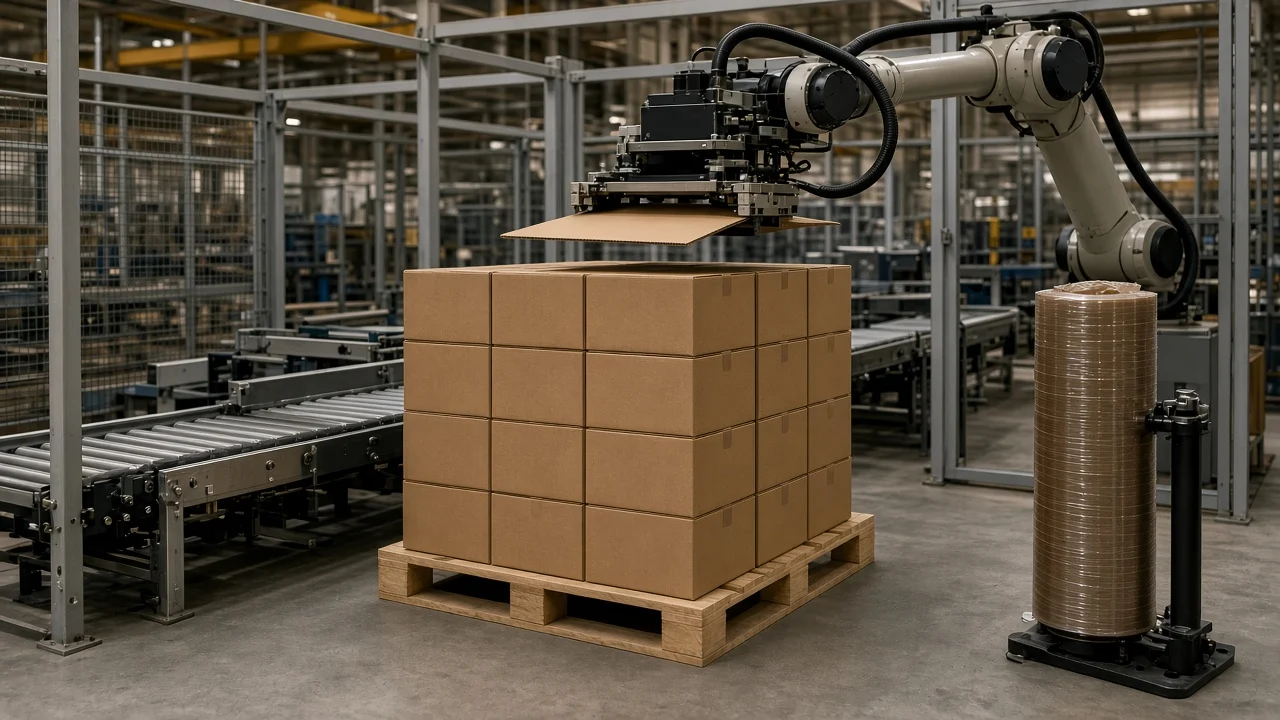
We did not park the palletizer as a separate island on the warehouse side. When the recipe changed, path, stack pattern, and stretch had to change together.
Application
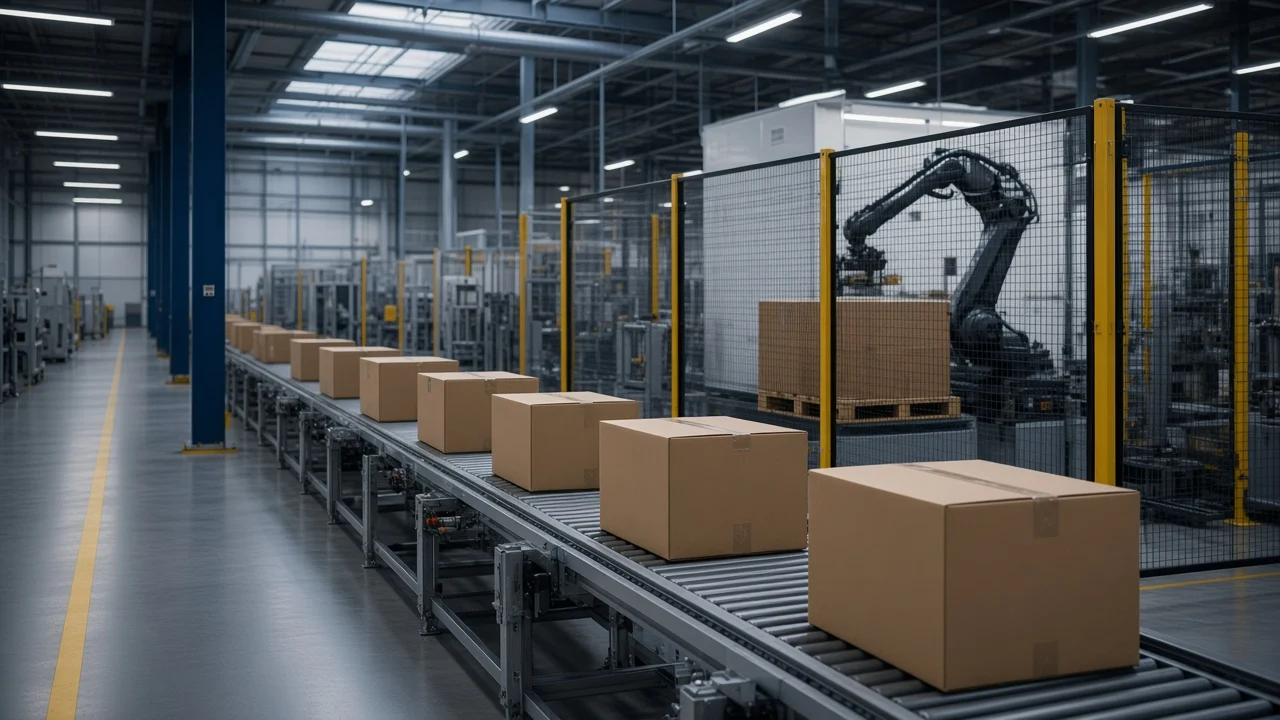
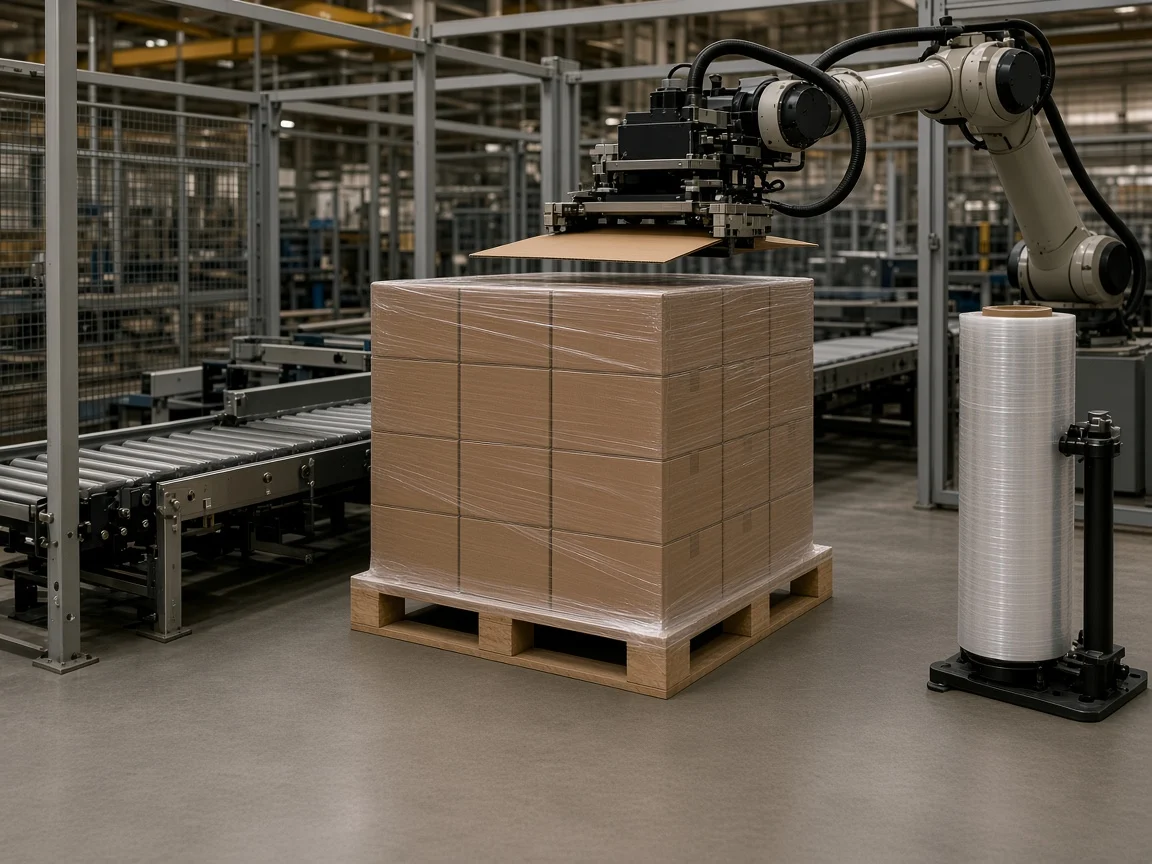
Three frames from box to outbound.
03 frames
01 / 03
Need
Tempo does not end when the box is finished.
The problem arrived as “a faster palletizer.” The real loss was a broken transfer and stacking without a recipe.
01
Product piles up
Stations keep up; the pallet does not. Shift end becomes a broken stack.
02
Pattern waits for the person who wrote it
When the box changes, stacking waits for that person. Stretch wrap stays in another world.
03
Outbound is disconnected
The pallet waits on an island at the end of the line. Dispatch transfer runs on guesswork.
Scope
What locked on this job.
- 01
End-of-line layout and buffer
- 02
Recipe-based pallet pattern and gripper
- 03
Automatic stretch wrap and outbound transfer
- 04
Box-arrival signal and line interlock
- 05
Product changeover on the HMI
Approach
The pallet continues the transfer.
Buffer and arrival signal were read first. The robot did not stand there as warehouse work left behind the line.
- 01
Flow
Box arrival, buffer, and cell interlock were written in the same sequence.
- 02
Recipe
Stack pattern and stretch wrap change with the product on the HMI.
- 03
Outbound
The wrapped pallet was left tied to the dispatch transfer.
On site
Stretch wrap is not the cell’s last job.
The robot places, the wrapper takes over, the outbound conveyor takes the pallet. All three speak in the same recipe.
Services
Services used.
- 01Review
Robotic Automation
A robot is not a cell until it locks to the line rhythm.
- 02Review
Line Automation
A running station is not a running line.
- 03Review
PLC & SCADA
Control software must belong to the night shift as well.
Result
The new production flow runs the length of the line.
Pallet quality is not a shift story. It is part of the recipe.
New production flow
Box, stacking, and stretch wrap run in the same sequence.
Completed equipment
Palletizing cell, wrapper, and outbound transfer were left together.
Process scope
Product changeover is on the HMI; the path is not a separate work order.
Projects
Talk with the engineering team.
A new line, an existing cell, or an ageing cabinet. Scope comes from the work on your line, not from a catalogue.