Yükleniyor
Yükleniyor
Yükleniyor
Yükleniyor
Services · 03
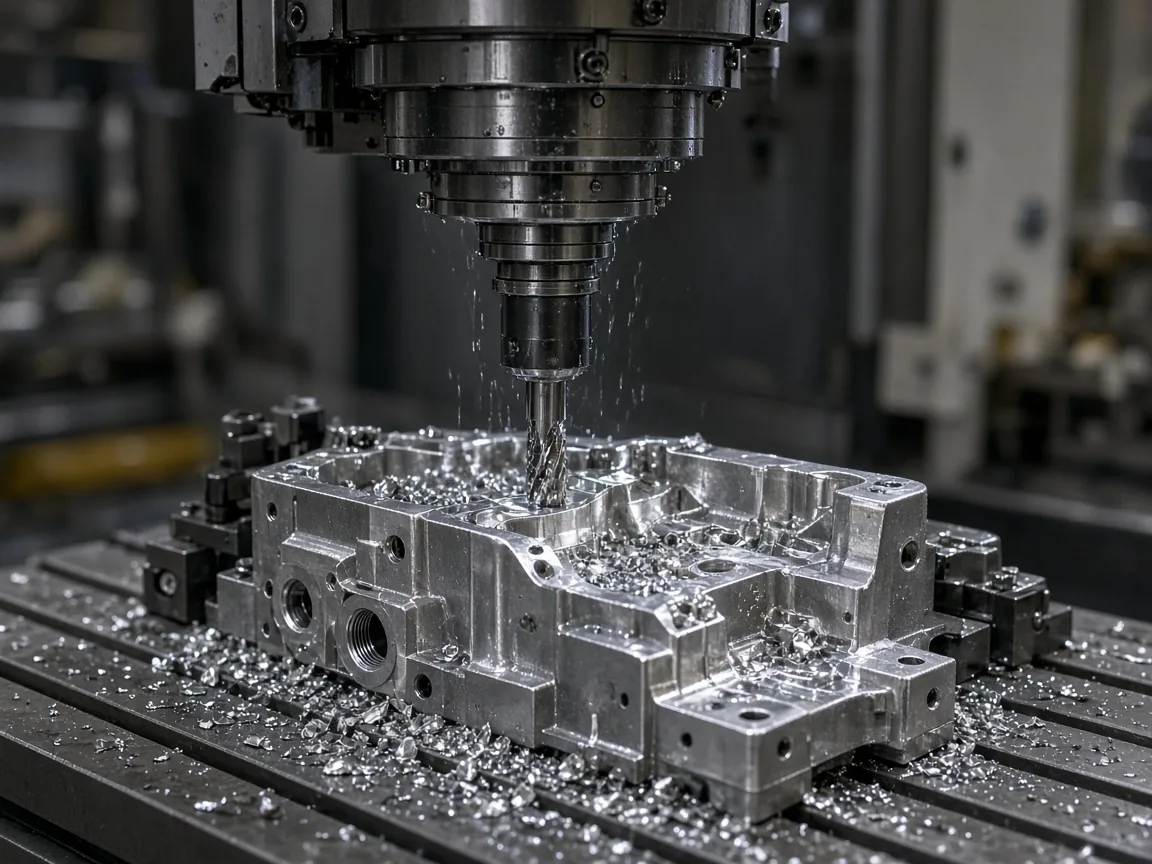
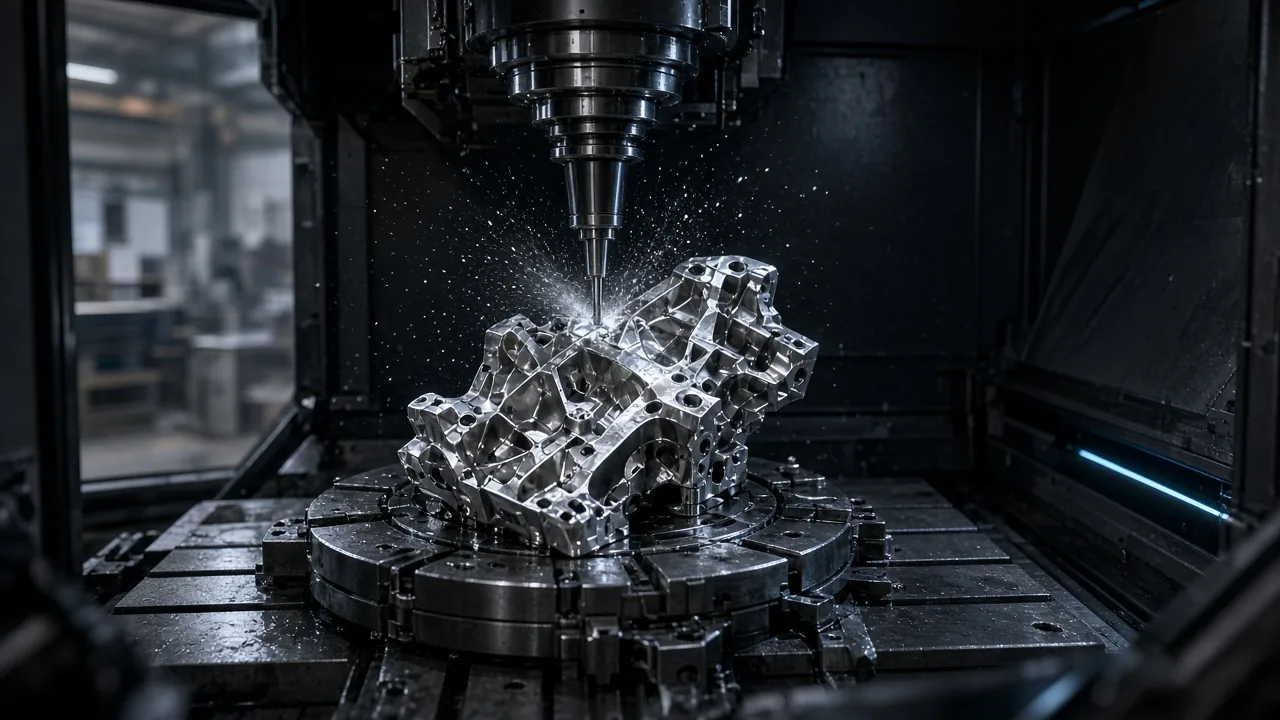
Intersecting ports, undercuts, and multi-angle connections close in one clamping. The goal is not showcasing the machine — it is cutting drift.
Service
Sequential rotations in three-axis work open the position chain. 5-axis holds the part once and brings the tool to the surface. Not every part needs continuous interpolation; 3+2 or simultaneous motion is chosen by geometry.
Short tooling, collision control, and fixture envelope are discussed before machine labels.
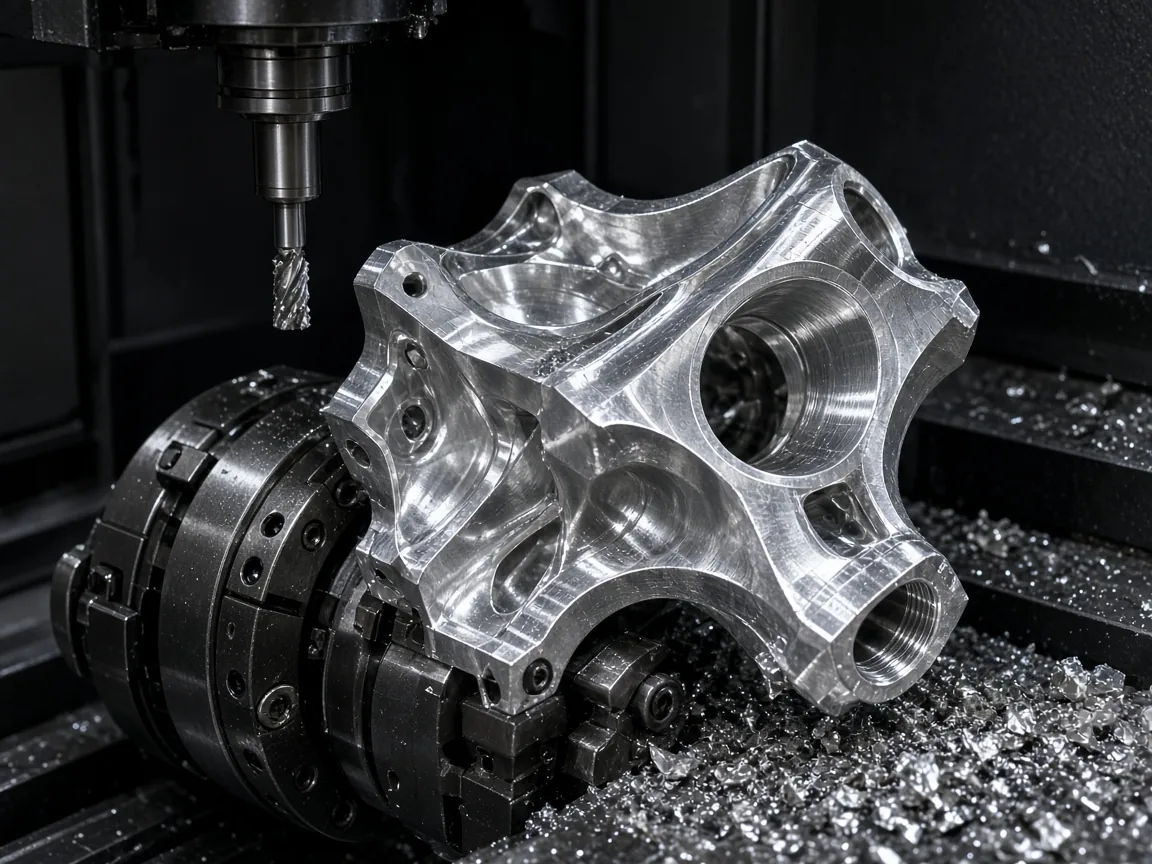
Undercuts and angled ports stay in the same clamping.
Approach
Simulation, tool length, and fixture envelope close before programming. The goal is not a showy toolpath — it is rigid cutting with short tools and repeatable position.
Validate on the first bodyCritical angled faces are sequenced to close in the same setup.
Long tools increase deflection. Tilt is used to shorten the tool.
Flat faces move with 3+2; flow surfaces use simultaneous when required.
Problem
Reference drift accumulates at every rotation. Angled bores and sealing faces split across stations and leak-tightness stays on the drawing. 5-axis opens to cut that accumulation — it is not the default machine for every job.
Scope
Intersecting faces, pockets, and outer contour.
Angled flange, cross bore, gasket seat.
Port, channel, and transition radius.
Collision, tool length, 3+2 selection.
Application
Turbo flow body
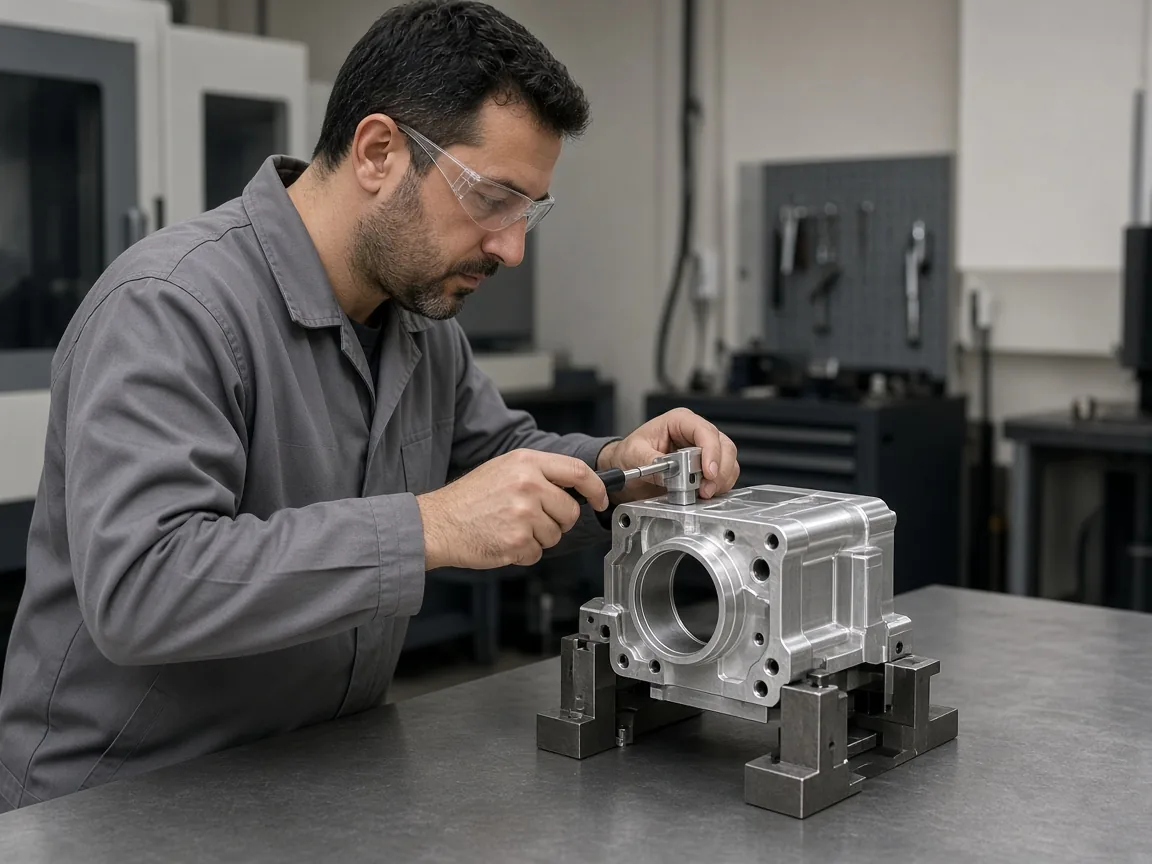
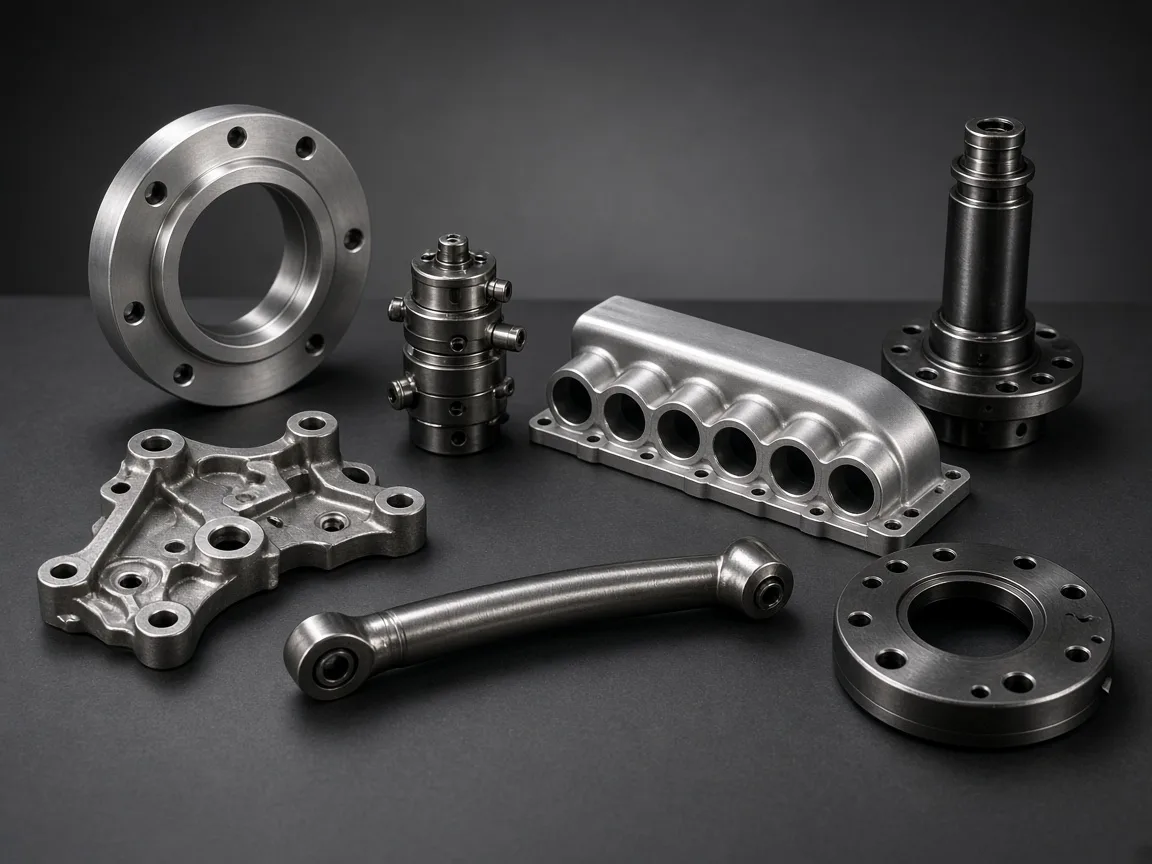
A multi-port aluminum body was machined in 5-axis for an automotive supplier. Three angled connections closed without splitting into separate setups. After the first body was measured, the same toolpath was written to the serial card; 3-axis milling remained only for the flat gasket face.
Process
01
Whether angled faces close in 3-axis is reviewed.
02
Fixture, tool length, and collision are simulated.
03
Port position and sealing face are measured.
04
Approved path moves to prototype or series.
Industries
5-Axis Machining rarely runs alone. Geometry and quantity open the adjacent line.
If you have angled surfaces, undercuts, or multi-port bodies, we review together whether single-setup machining is required.