Yükleniyor
Yükleniyor
Yükleniyor
Yükleniyor
Services · 02
Pockets, covers, and mounting surfaces are written to the same datum. Unnecessary second setups are not opened; vent paths and threads do not scatter across stations.
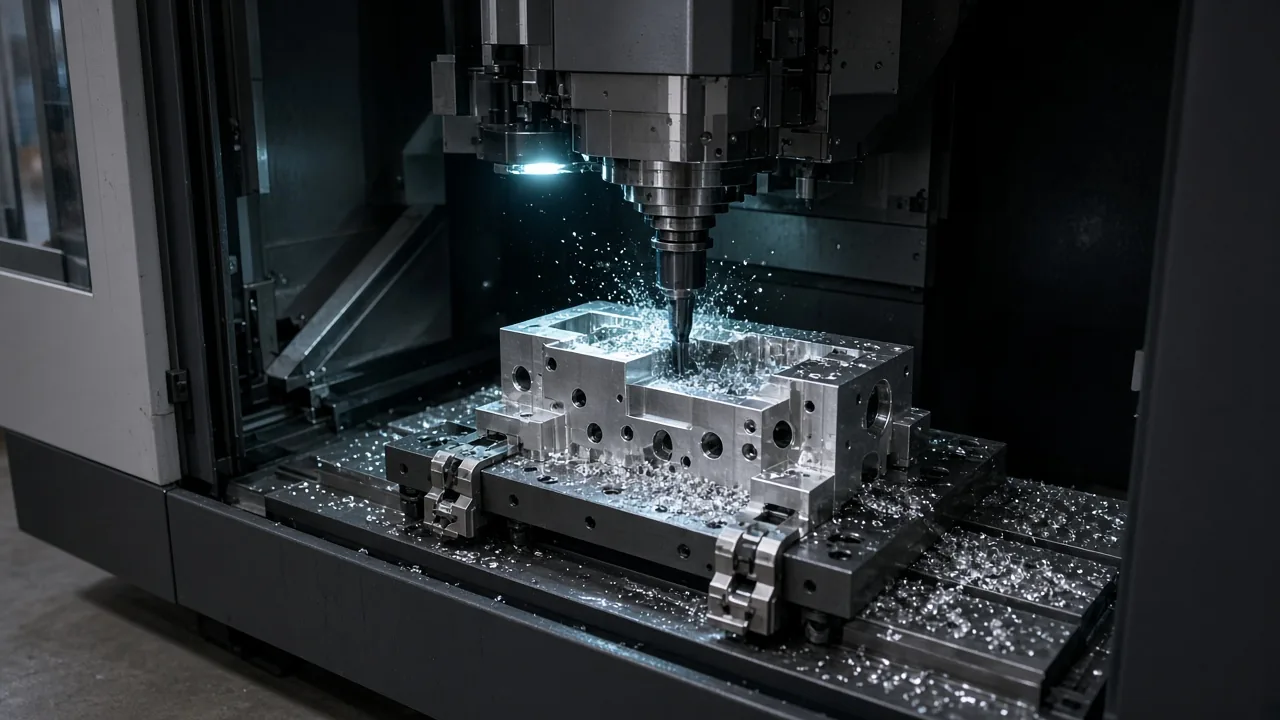
Problem
When a multi-face part shifts at every setup, flatness and positional tolerance stay on the drawing. Vent paths, threads, and pockets split across machines and the assembly surface fails. Milling is not opening as many stations as there are faces.
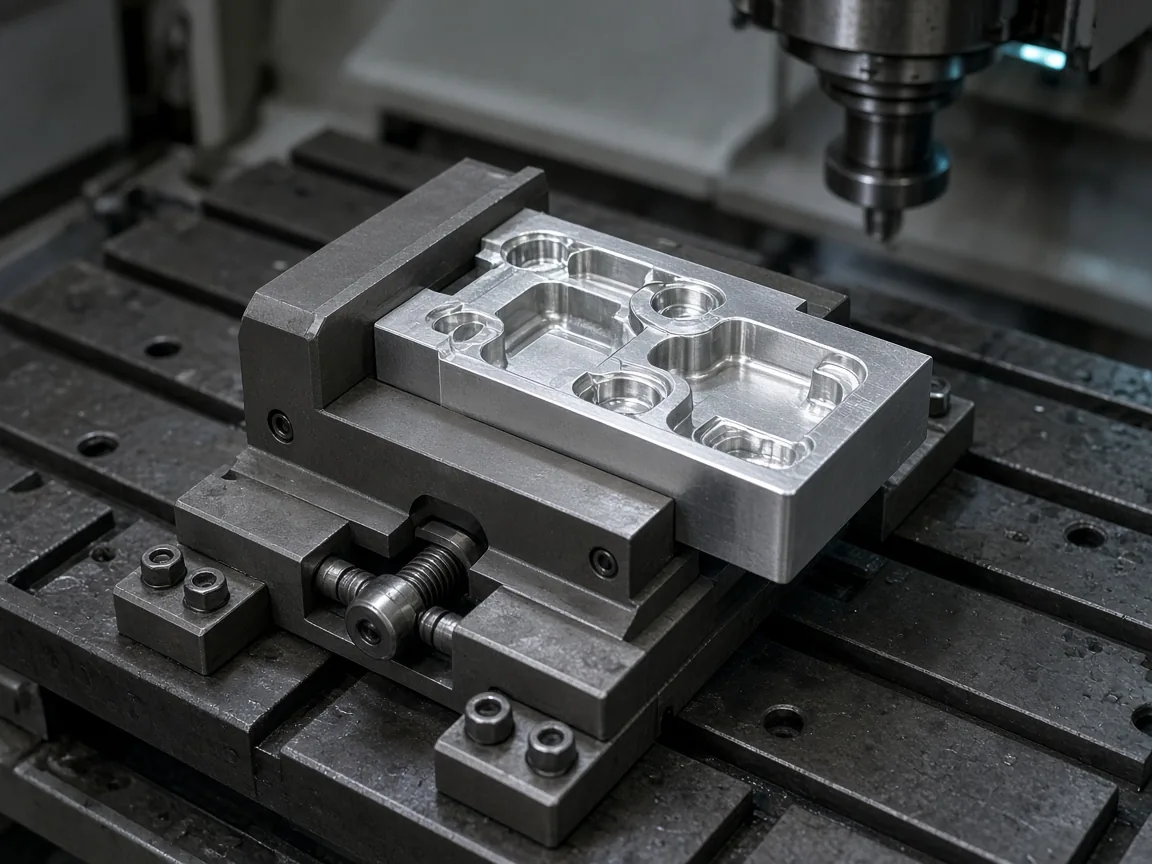
Service
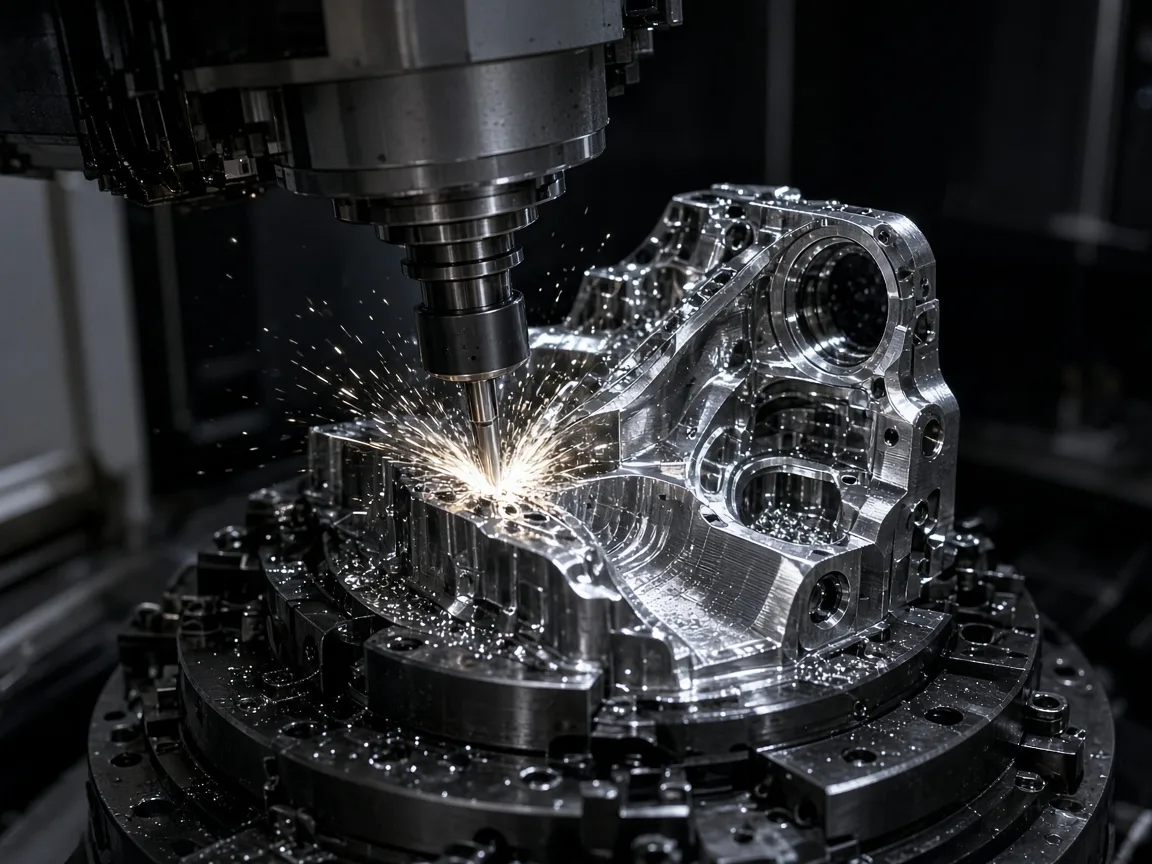
Covers, bodies, and mounting plates are opened on a vertical machining center. Pocket geometry, cooling channels, and threads are preserved through plate strategy and operation order.
The goal is not more tool changes — it is locking the datum face once and writing remaining geometry to that reference. When an undercut or angled port appears, the job moves to 5-axis with intent.
Approach
The first station locks the datum. Pockets and vents open to that reference; threads and secondary faces come last. Collision and tool length are reviewed with fixture height.
Material and machine rangeFlat reference and pin/bore location close in the first setup.
Rough and finish pockets, chip evacuation, and corner radii run on the same plan.
Threading and secondary faces sequenced so they do not break the datum.
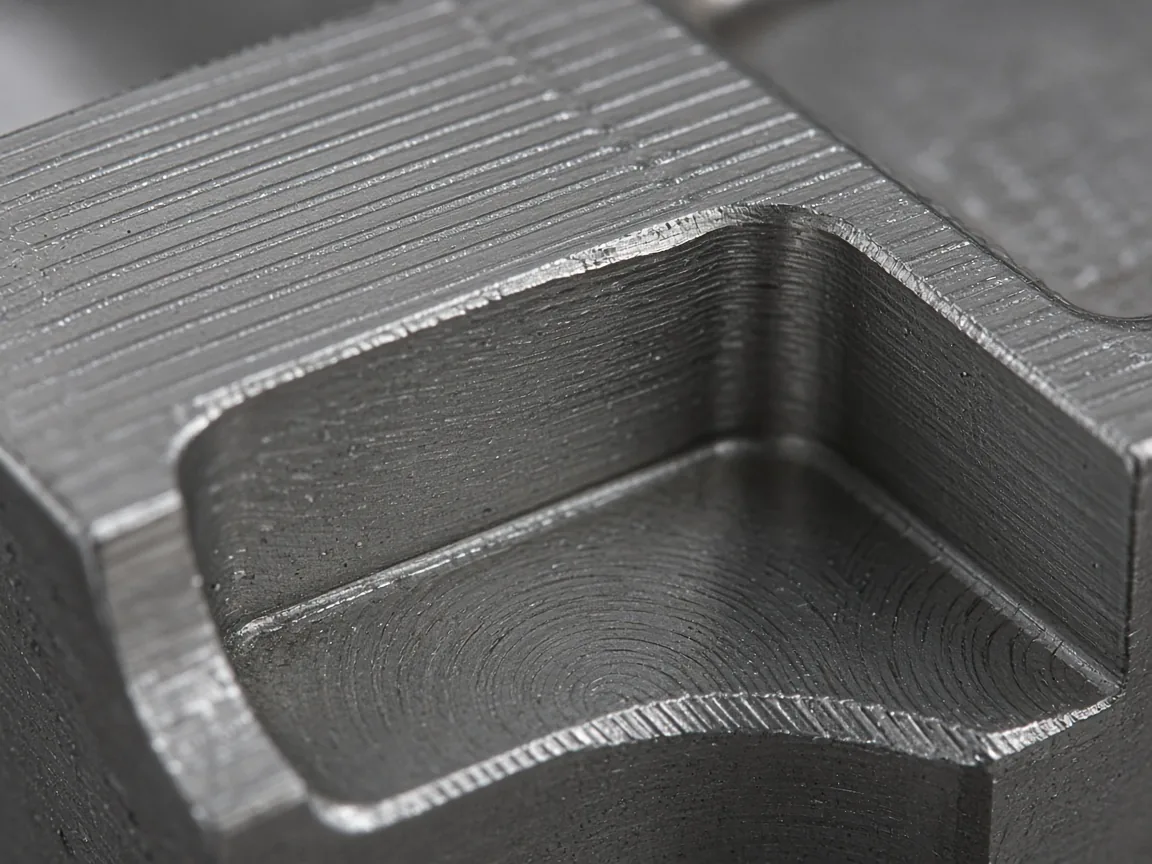
Scope
Milling carries non-rotational surfaces and mounting planes. Shafts stay on the turning line.
Assembly face, gasket seat, and cover mating.
Fixture plate, pin bore, flat reference.
Blind pockets, vent channels, threading.
Channels, fins, and sealing surfaces.
Industries
Process
Which face is datum and which needs a second setup is written down.
Vise, pin, or custom fixture is selected.
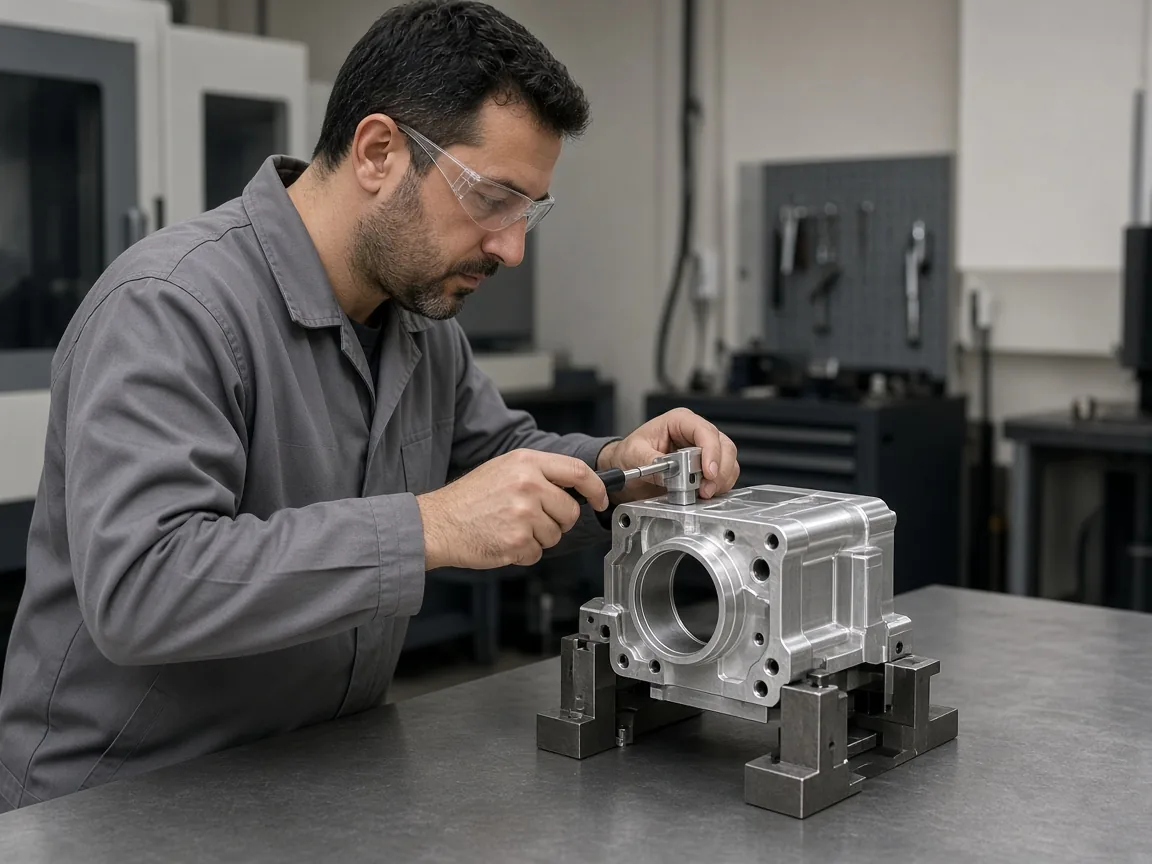
Flatness and position are checked with mounting holes.
Approved sequence moves to prototype or serial card.
Application
Drive cooling enclosure
An aluminum enclosure was machined for an electronic drive. The gasket plane was locked in the first station; cooling channels and threaded connections were written to that datum. No undercut appeared, so 5-axis was not opened — the job closed on the milling line.
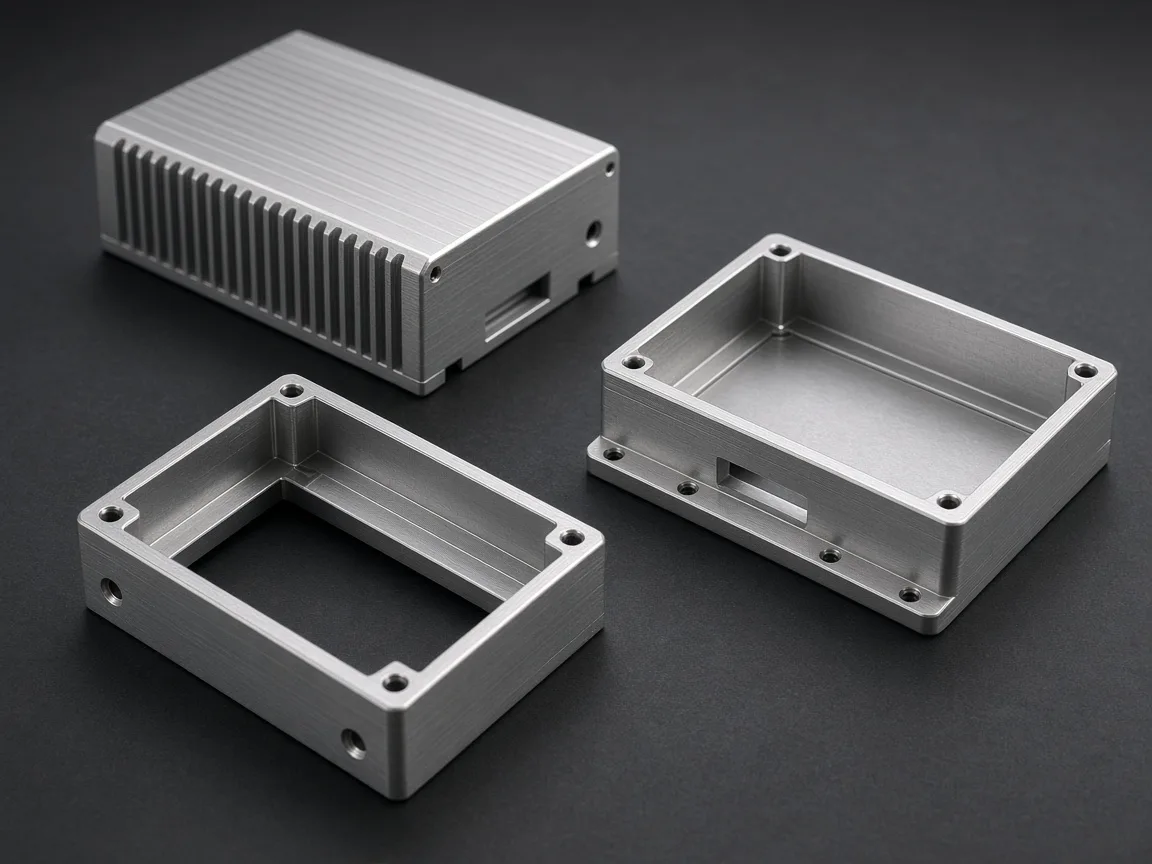
CNC Milling rarely runs alone. Geometry and quantity open the adjacent line.
Send the body, cover, or plate file. We lock datum and operation sequence together.