Yükleniyor
Yükleniyor
Yükleniyor
Yükleniyor
Projects · 06
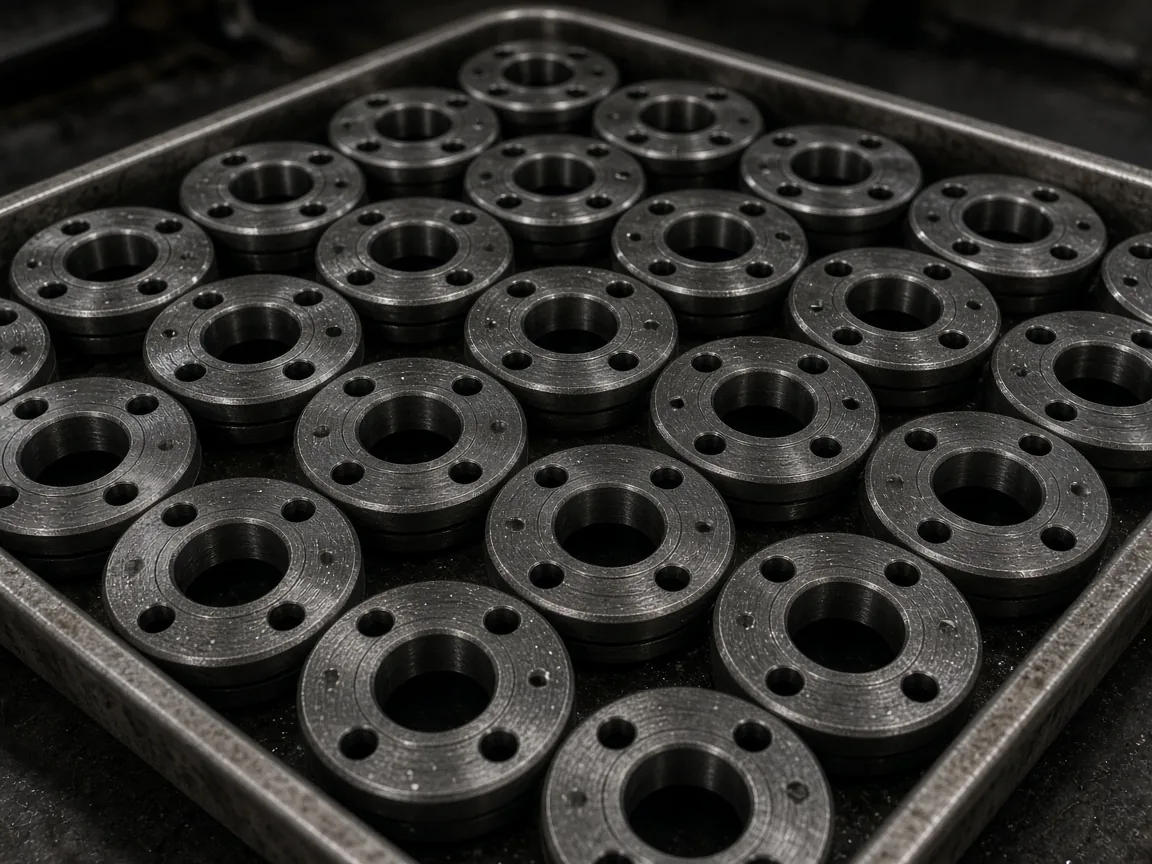
Face and bolt circle stayed the same on the tray.
Project
Repeat OEM connection flange in Manisa. Bolt circle and bore had to be written to the same turning face reference. As batch grew, face runout became where the line stopped.
Requirement
Face runout and hole circle drifted without tool life tracking. Delivery window held on last flange in tray, not first. Repeat order broke when vise changed.
Kapsam
Scope was not a single flange but repeat batch with identical trays.
Flange batch
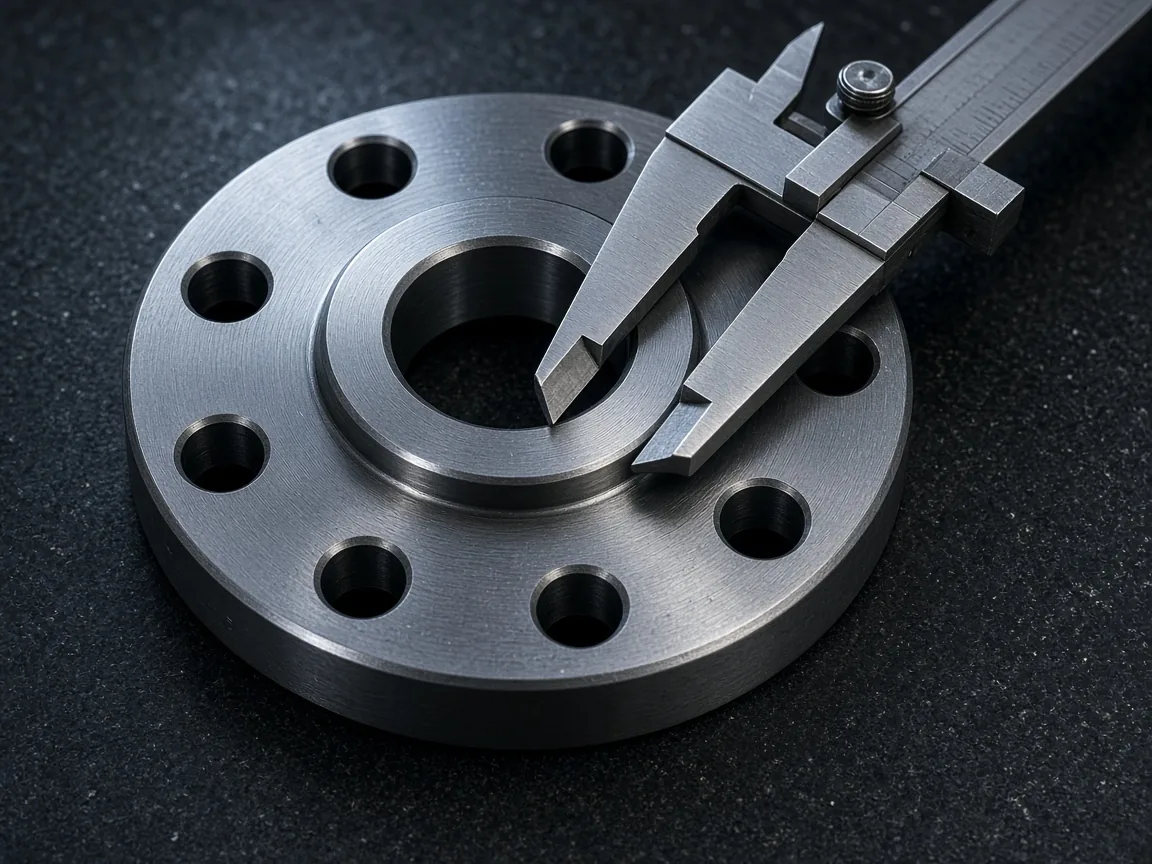
Face, bore, and bolt circle on the same card.
Face reference
Chuck takes face plane as datum.
In-process check
Circle and face checked at every tool change.
Repeat order
Vise and program version unchanged.
Yaklaşım
In-process check at every tool change. Vise and program held on repeat order. Last flange on tray had to carry first flange circle.
Repeat the line needed held on the card.
Flanges on tray carried the same hole circle. OEM connection read last part like first. Repeat order opened with same vise.
Datum
Face plane became chuck reference. Bore written to this plane.
Check
Circle and face measured at tool change.
Lock
Vise and program copied, not reopened, on next batch.
Görseller
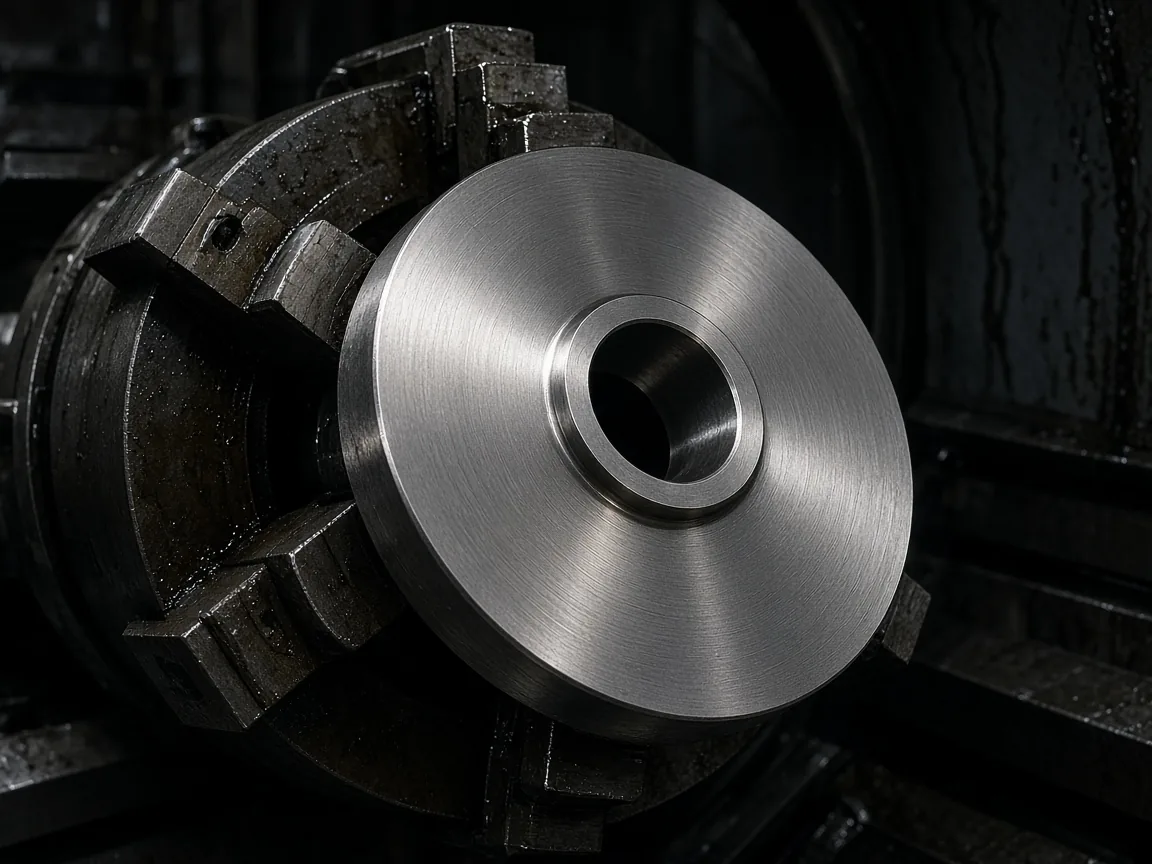
Face, circle, and locked tray—three surfaces where the flange repeats.


01 / 03
Face plane
Kaydırarak diğer bakışları görün.


Outcome
Connection flange flow deployed. Face and hole circle held on tray. Repeat order did not search for new vise.
New production flow
Flange batch with in-process check at tool change.
Deployed solution
Locked turning job card and unchanged vise.
Integrated system
Face, bore, and bolt circle on the same reference.
Process scope
Repeat OEM flange, tray, and measurement record.
Kullanılan çözümler
Flange closed as face reference and locked series on the same job.
If face and hole circle must hold on the tray, we lock vise and program from the start.