Yükleniyor
Yükleniyor
Yükleniyor
Yükleniyor
Projects · 02
Bearing diameter held with grinding allowance.
Project
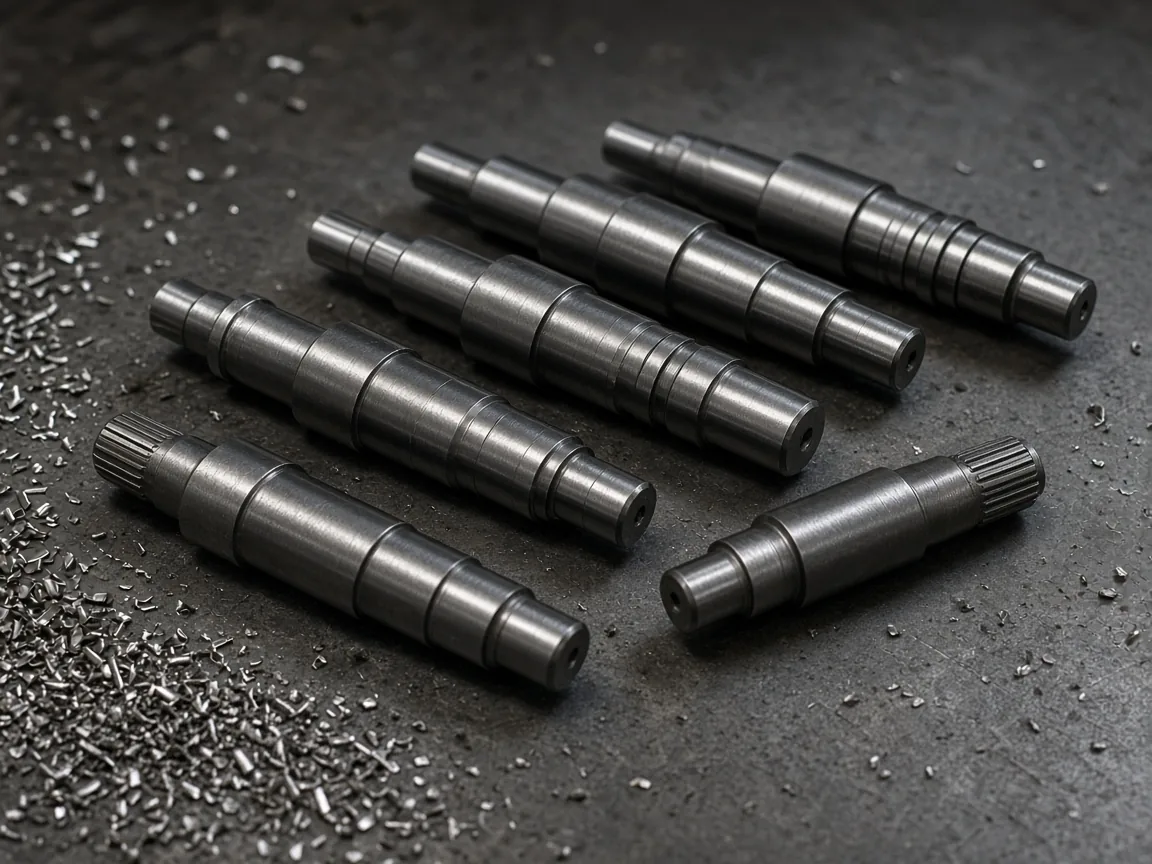
Stepped reducer input shafts for a machinery OEM in Kocaeli. Concentricity, face, and keyway slot had to come from the same turning reference. Long shaft was not left to a second setup.
Requirement
When the shaft was re-clamped, the journal ran hot. If grinding allowance was left without a station, the next line step drifted. Keyway had to open without breaking the turning datum.
Kapsam
Scope was not a single shaft but a shaft group carrying the same allowance on spare batches.
Stepped shaft
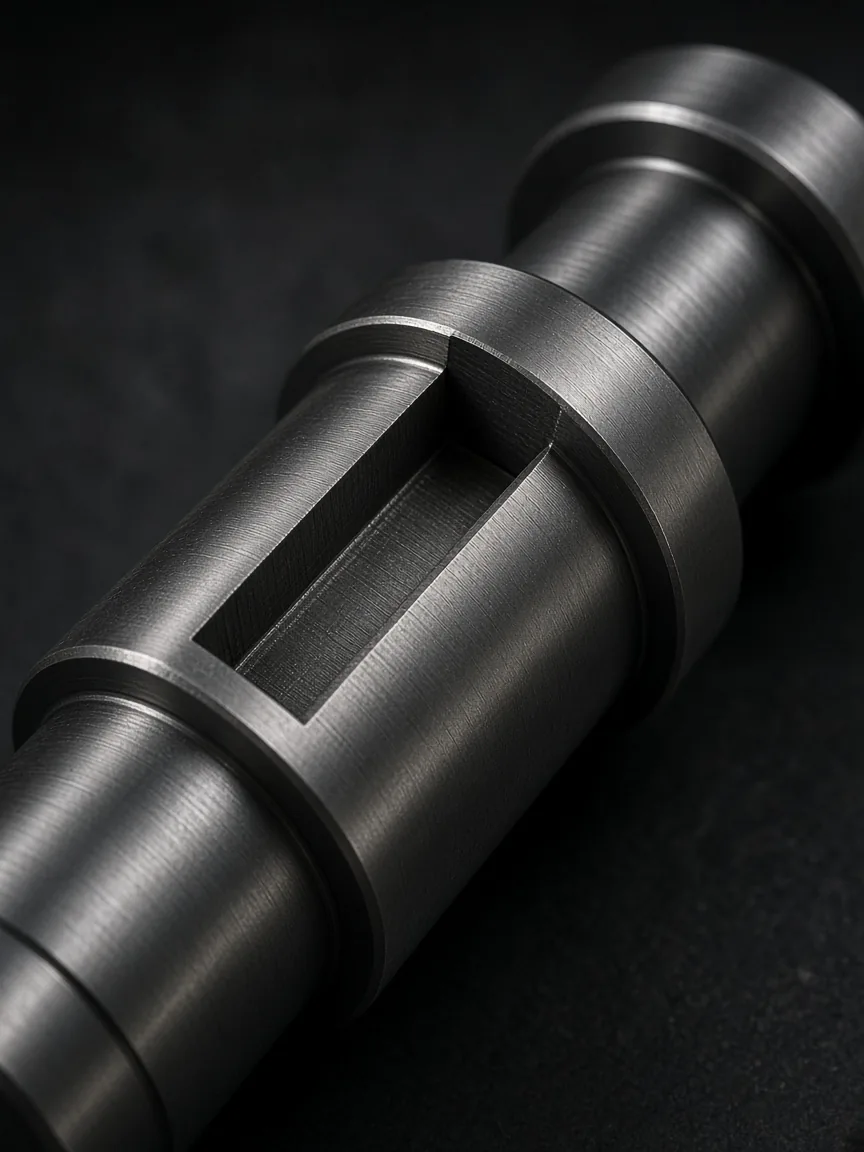
Journal, shoulder, and keyway on the same diameter chain.
Live center
Second support on long shaft to cut deflection.
Keyway note
Milling opens the slot without breaking the turning reference.
Grinding allowance
Allowance written on the job packet. Next line step stays in station.
Yaklaşım
Shaft length called for a second setup. Live center engaged; keyway routed to mill with turning datum preserved on documentation.
Reducer recognized the shaft on spare batch too.
After first shaft measured, job card locked. Spare batch delivered same allowance and concentricity. Journal heat closed without second setup.
Chuck
Diameter chain closed in one context. Shoulder and journal on the same card.
Center
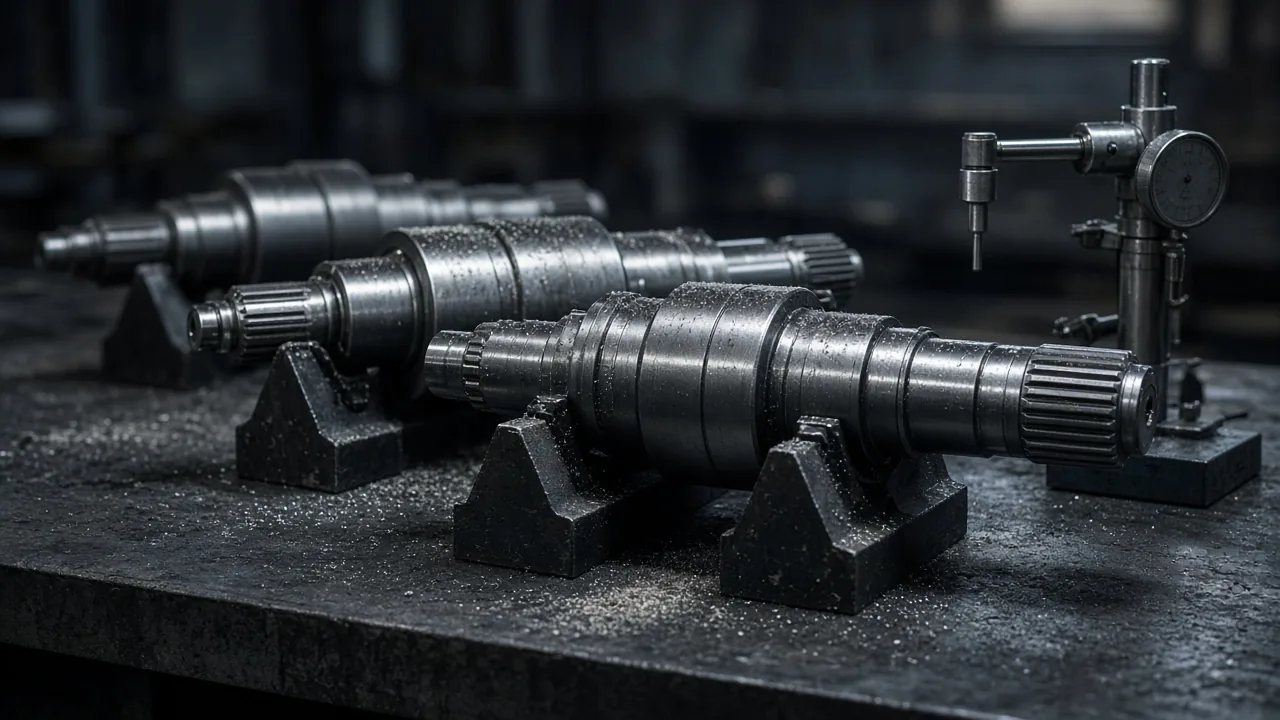
Live center on long shaft. Deflection not left to second jaw.
Keyway
Slot opened on mill. Turning reference held on the packet.
Görseller
Chuck, keyway, and measurement—three stations where the shaft group stopped.
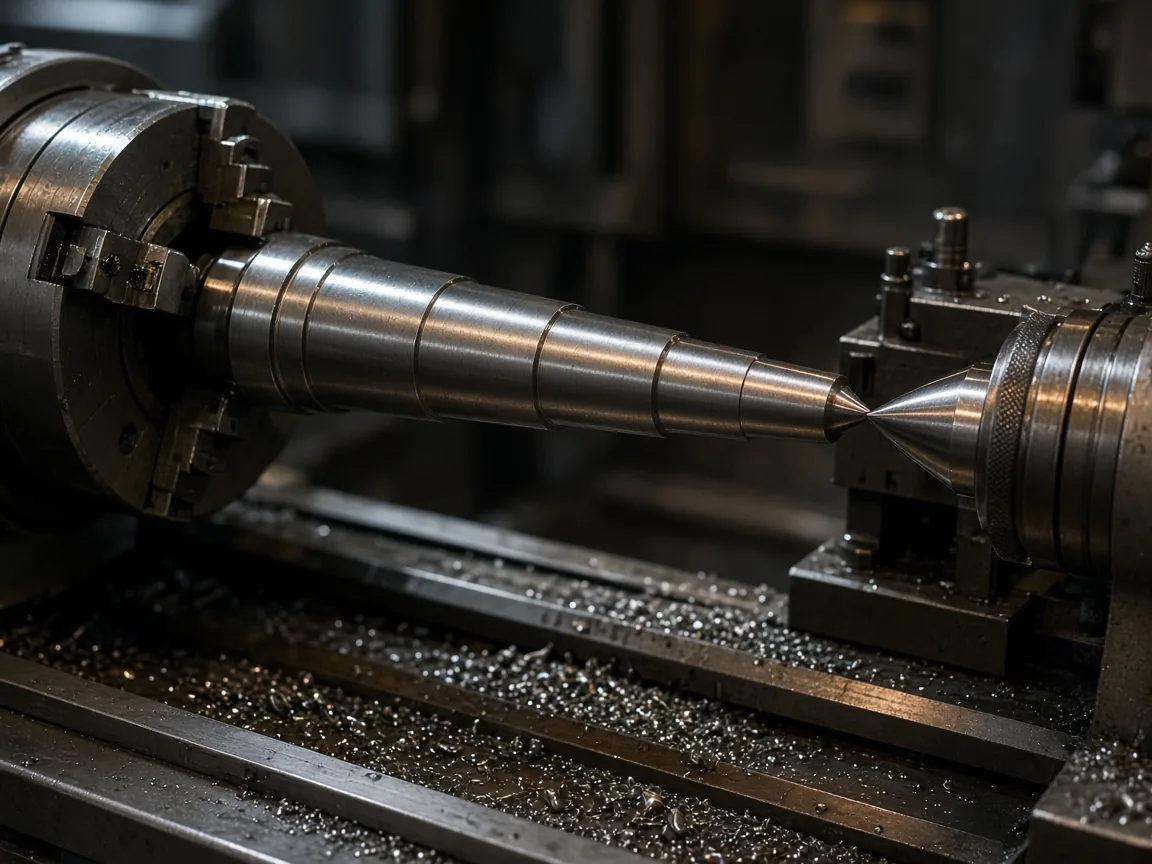


01 / 03
Live center
Kaydırarak diğer bakışları görün.


Outcome
Input shaft set delivered to the reducer line. Grinding allowance held on documentation. Concentricity closed without splitting into second setup.
Completed equipment
Stepped input shaft group with spare batch.
Integrated system
Turning diameter chain and milled keyway on the same datum.
Deployed solution
Locked shaft job card and documented grinding allowance.
Process scope
Journal diameter, face, keyway slot, live center.
Kullanılan çözümler
Shaft group closed with turning and milling on the same datum.
If journal diameter and keyway must sit on the same reference, we write grinding allowance on the packet from the start.