Yükleniyor
Yükleniyor
Yükleniyor
Yükleniyor
Projects · 04
Cover seated on the gasket plane.
Project
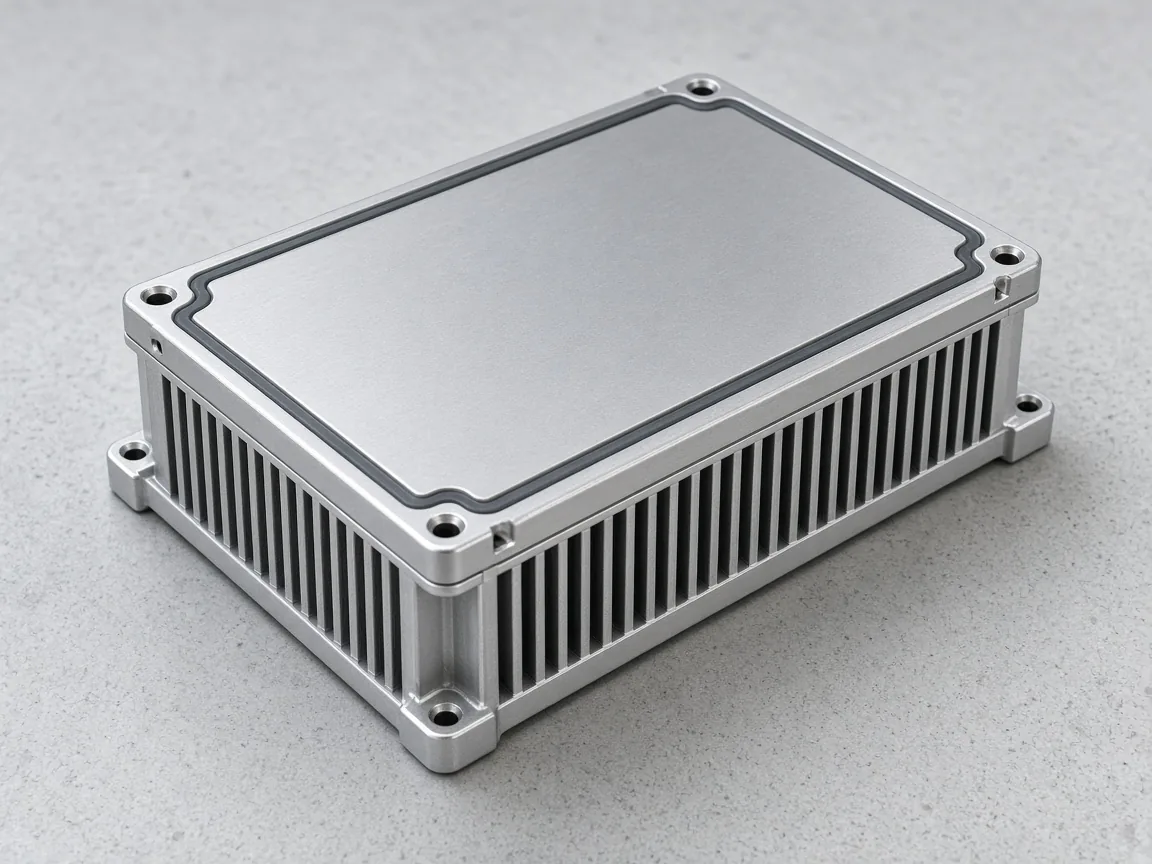
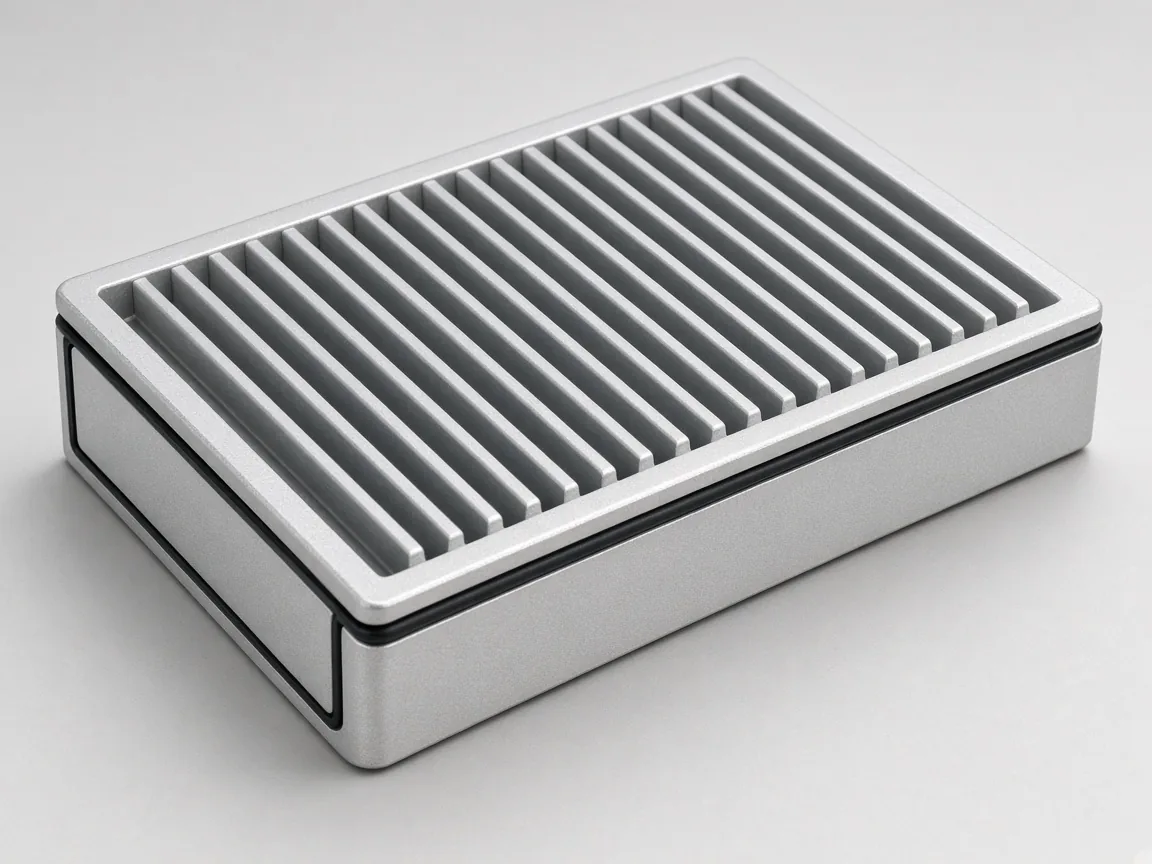
Finned aluminum cooling enclosure for a controls OEM in Ankara. Pocket, bolt pattern, and seal groove split across stations meant cover would not seat on body. Series did not open until first part seen in assembly.
Requirement
Pocket and threads split across setups meant cover would not seat on body. Thin wall vibrated without written toolpath. Cooling assembly looked for seal plane at build.
Kapsam
Scope was not heat distribution but the enclosure where cover seats and the approved first part.
Cooling body
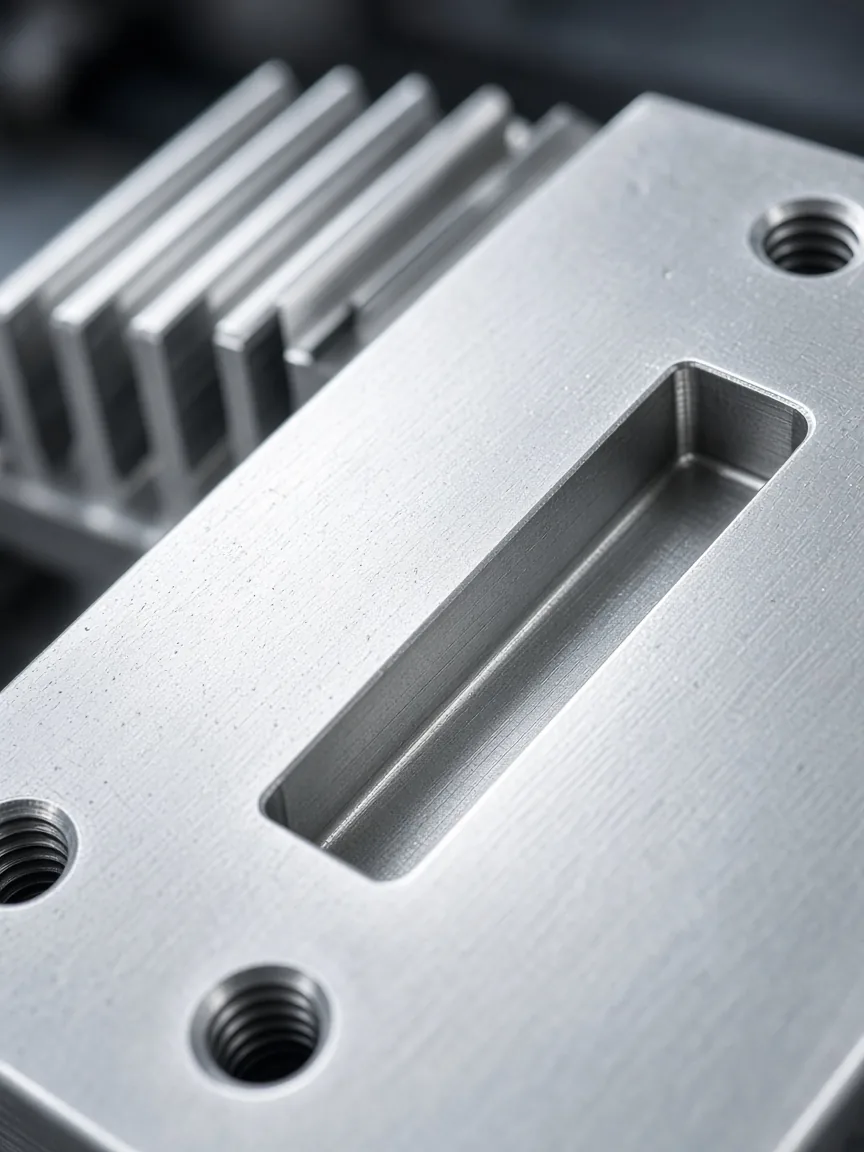
Fin and pocket on the same milling plate.
Seal groove
Groove holds on the same datum as cover plane.
Bolt pattern
Hole circle does not drift from body reference.
First part
Batch job card not written until assembly seen.
Yaklaşım
First enclosure came out in series 6xxx. Feed rate written for thin wall. Second part not opened until cover seated on seal plane.
Drive received enclosure with cover.
Approved toolpath carried to series. Wall feed unchanged. Cover seated on seal plane; drive body did not search for a second station at assembly.
Plate
Fin, groove, and bolt pattern in one milling setup.
Wall
Toolpath written for thin wall. Vibration seen on table.
Assembly
Series job card not locked until cover seated.
Görseller
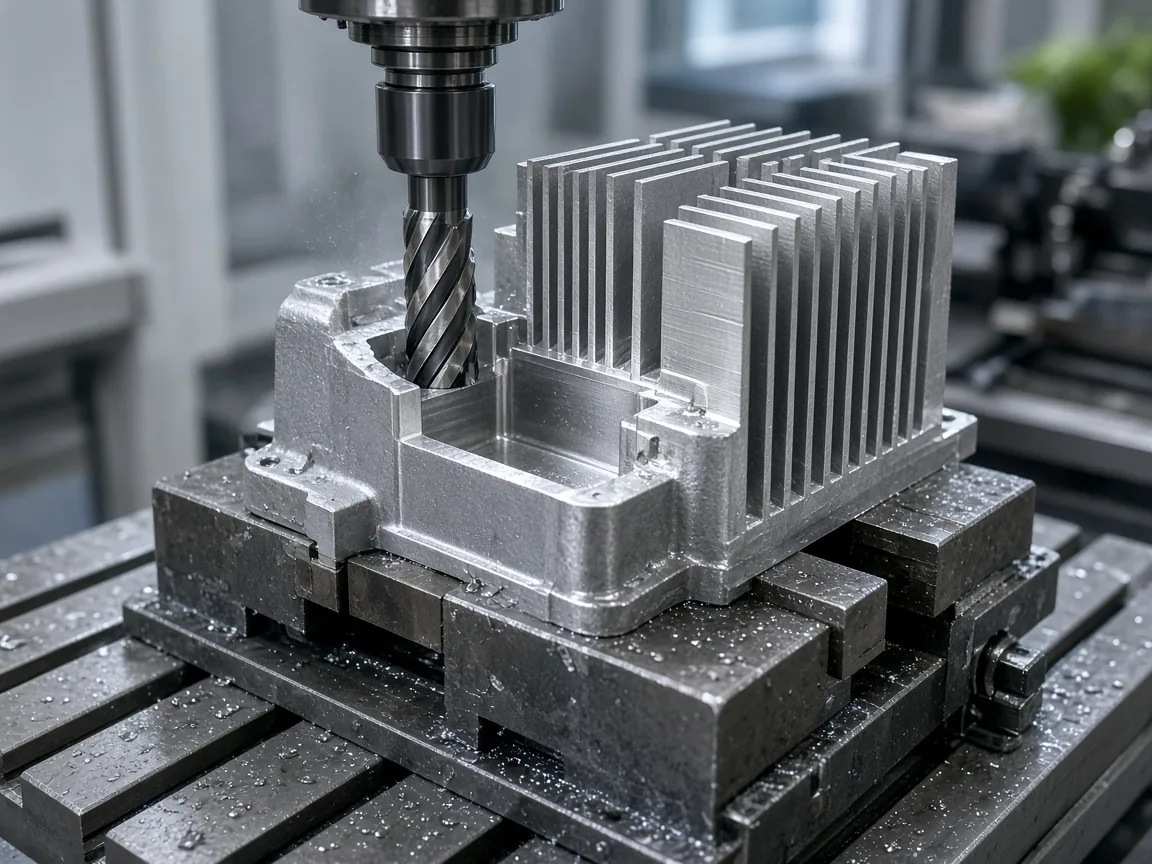
Milling, groove, and seated cover—three faces of the enclosure.


01 / 03
Milling plate
Kaydırarak diğer bakışları görün.


Outcome
Cooling enclosure delivered to drive assembly. Approved toolpath carried to series. Seal plane not split to second station.
Completed equipment
Finned enclosure and seated cover plane.
Integrated system
Fin, seal groove, and bolt pattern on one datum.
Deployed solution
Approved toolpath and wall feed rate.
Process scope
First-part assembly and milling card carried to series.
Kullanılan çözümler
Enclosure closed as milling and first-part approval on the same job.
If cover must seat on the seal plane, we hold groove and bolt pattern on the same plate.